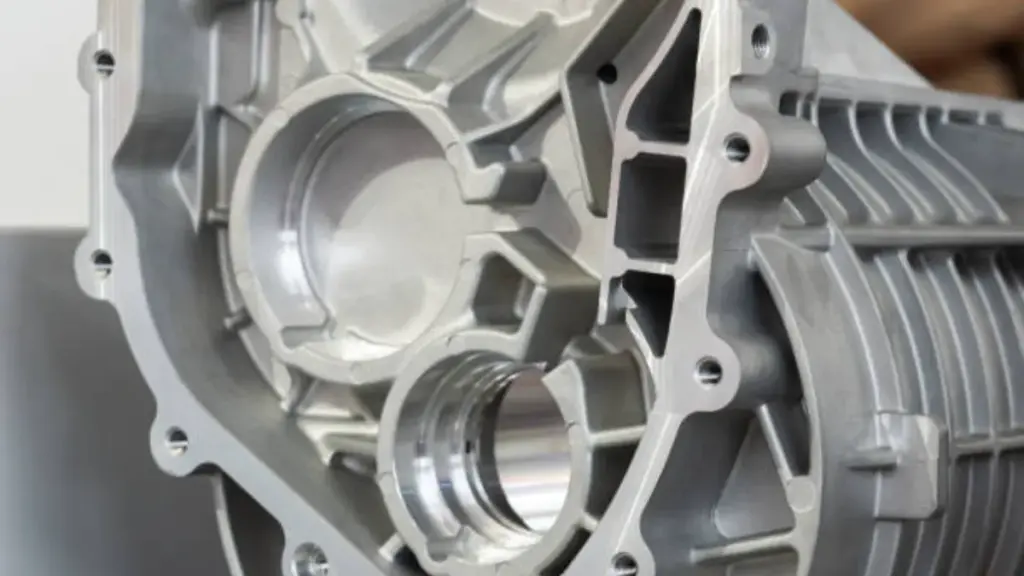
Anodizing and powder coating both protect an aluminum die casting. They do it in opposite ways. One grows the surface itself into a hard oxide; the other lays a polymer film on top. That difference decides how the part tolerates its own alloy, where its dimensions land after finishing, and whether the look survives years outdoors.
Sourcing teams comparing anodizing vs powder coating for die cast parts usually start with the wrong question, which finish is better. The right question is which failure each finish protects against. This guide gives the mechanism, the honest limits of each on cast aluminum, and a selection checklist you can run on a drawing in minutes.
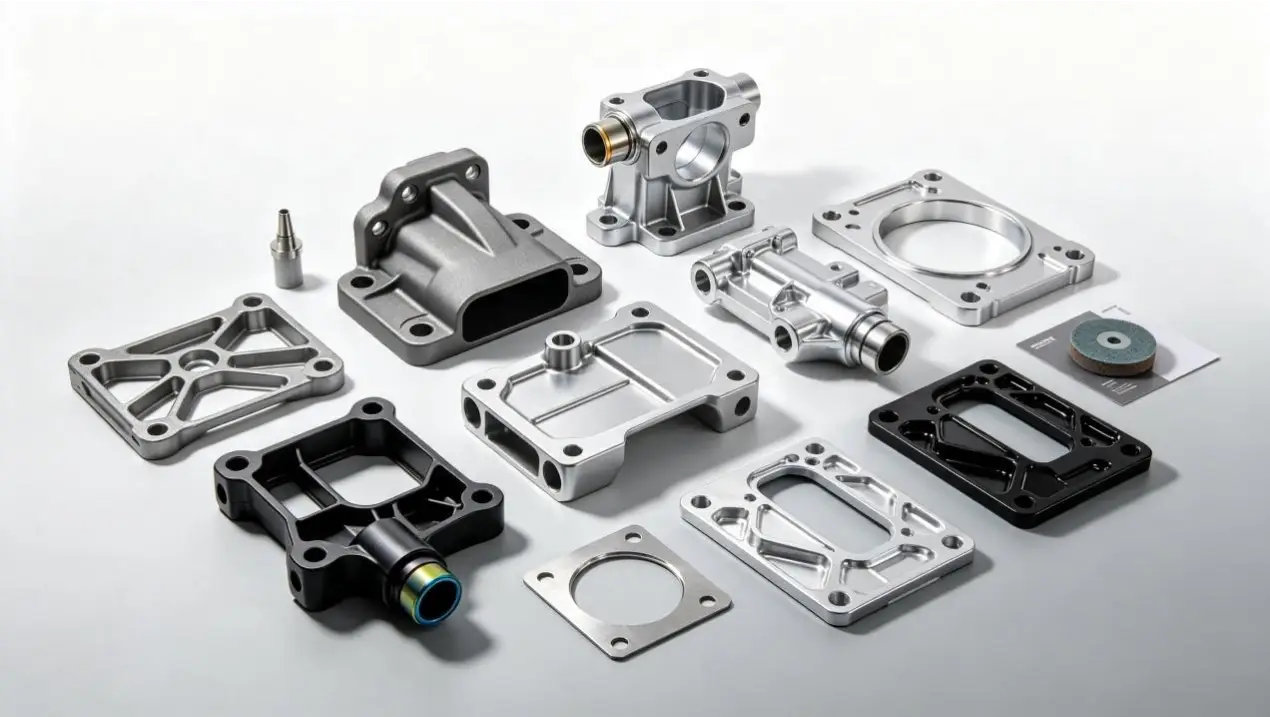
What Each Process Actually Does to the Metal
아노다이징 is an electrolytic conversion process. The part becomes the anode in an acid bath, and current grows a thick, ordered layer of aluminum oxide out of the substrate. Because the film is converted base metal, it is integral, so there is no interface for it to peel from. The porous film is then dyed and sealed. A typical Type II decorative film runs about 5 에게 25 미크론.
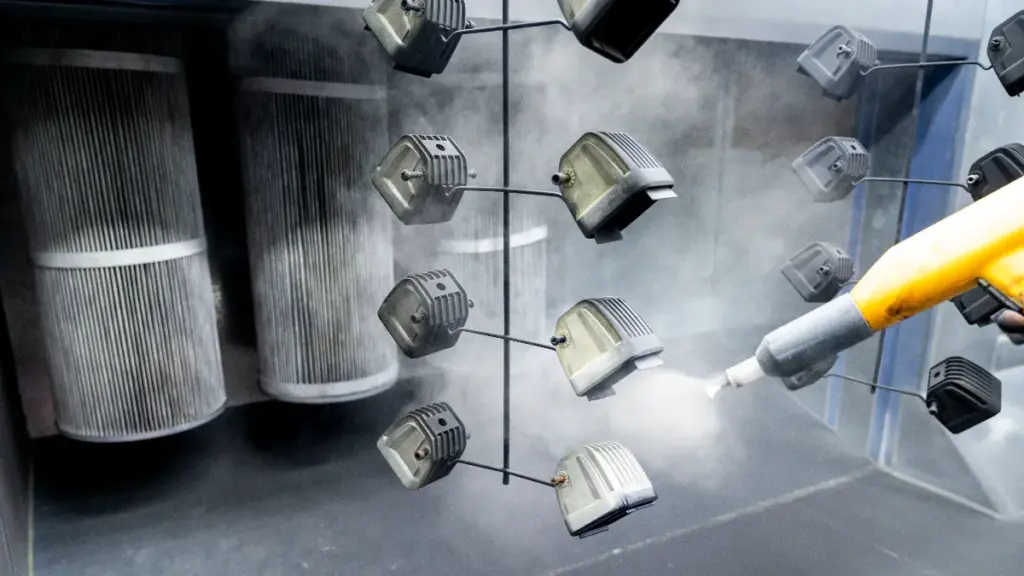
분체 도장 is an applied coating. An electrostatically charged polymer powder is sprayed onto the part, which is then baked so the powder flows and cures into a continuous film. Build thickness usually sits between 60 그리고 120 미크론, a real layer rather than a converted surface. The resin chemistry, epoxy or polyester, sets UV stability, 유연성, and chemical resistance, 으로 powder coating overview explains. Full color matching and textures from matte to gloss come with the polymer route.
Why Die-Cast Aluminum Complicates Anodizing
Here is the fact that surprises most teams: the silicon in common die-casting alloys does not anodize. ADC12 runs roughly 9.5 에게 12 percent silicon and A380 about 7.5 에게 9.5 퍼센트, and those silicon phases stay inert while the surrounding aluminum converts. The result is a finish that is typically gray, mottled, and slightly frosted. It reads as uniform in its lack of uniformity on functional housings, but it is nothing like the bright, predictable color anodizers get on low-silicon wrought stock. 그만큼 high-silicon anodizing guide covers that alloy behavior in detail.
That metallurgical reality splits the decision early. If the anodized look on the drawing was approved from a wrought sample, a die-cast ADC12 part will not match it, and no anodizer’s tweaks fix what the alloy causes. Teams who want true color consistency on a cast part usually end up on the coating route, and reserve the anodize look for castings where gray metal is the intent.
The Comparison That Decides It
The table below summarizes the trade-offs that decide most calls.
| Attribute | 아노다이징 | 분말 코팅 |
|---|---|---|
| Coating nature | Converted surface, integral | Applied polymer film |
| Typical thickness | 5-25 미크론 (Type II) | 60-120 미크론 |
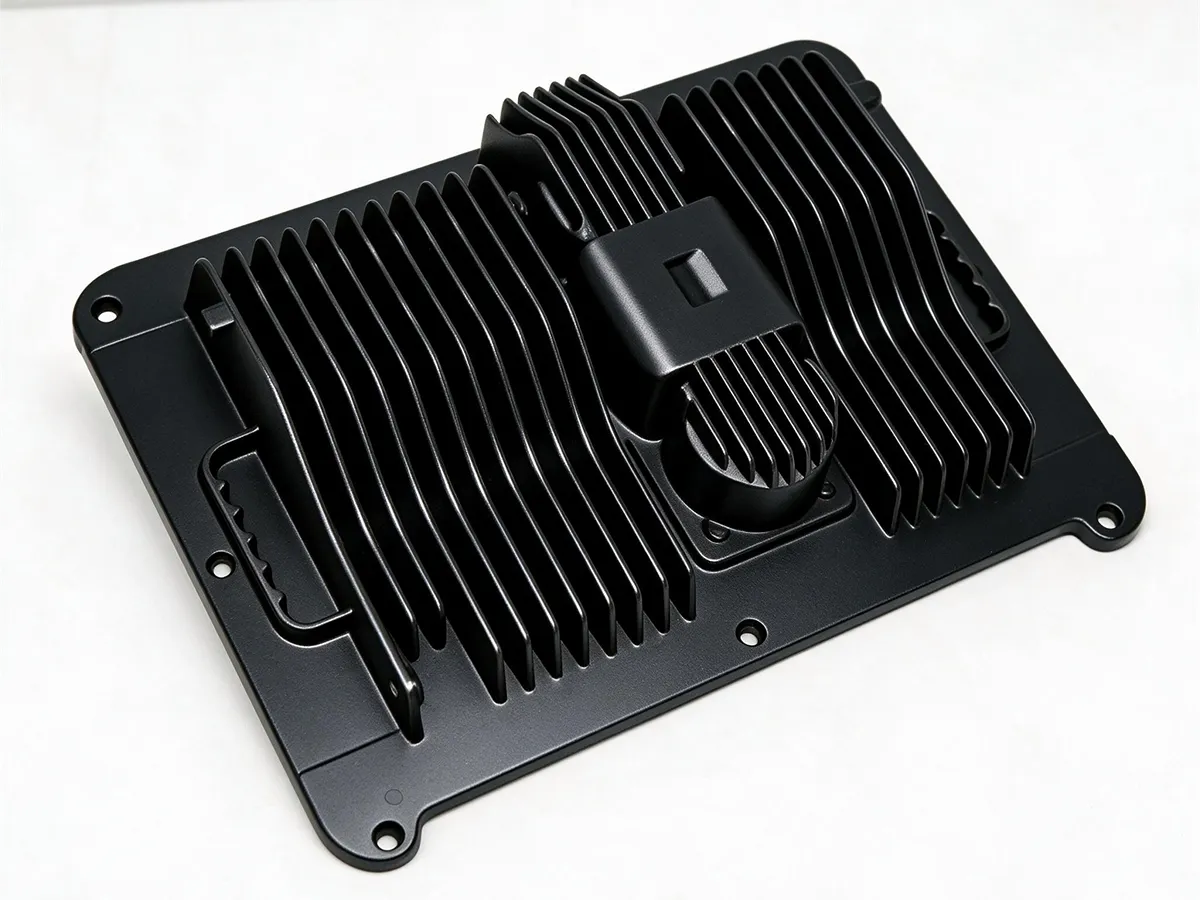
| Look on die castings | Gray, mottled from silicon | Full color, gloss and texture control |
| Corrosion and UV outdoors | Good when sealed; UV-stable film | 훌륭한; polyester chemistries rated for UV |
| Dimensional impact | Minimal; threads usually still work | Real; fits and threads need masking |
| Surface defects | Reveals porosity paths and die marks | Bridges and hides light defects |
Two rows deserve emphasis. On defects, anodizing is honest to a fault: porosity from the shot, flow lines from the cavity, and polishing marks all show. It runs as a quiet quality audit of the casting underneath. Powder is forgiving, since a 60-micron film spans small blemishes that anodize would broadcast. On dimensions, a 100-micron powder build on both faces of a slip fit adds 0.2 mm of interference. 스레드, press-fits, 결합 표면, and grounding points either get masked or get designed in from the start.
When Powder Coating Is the Right Call
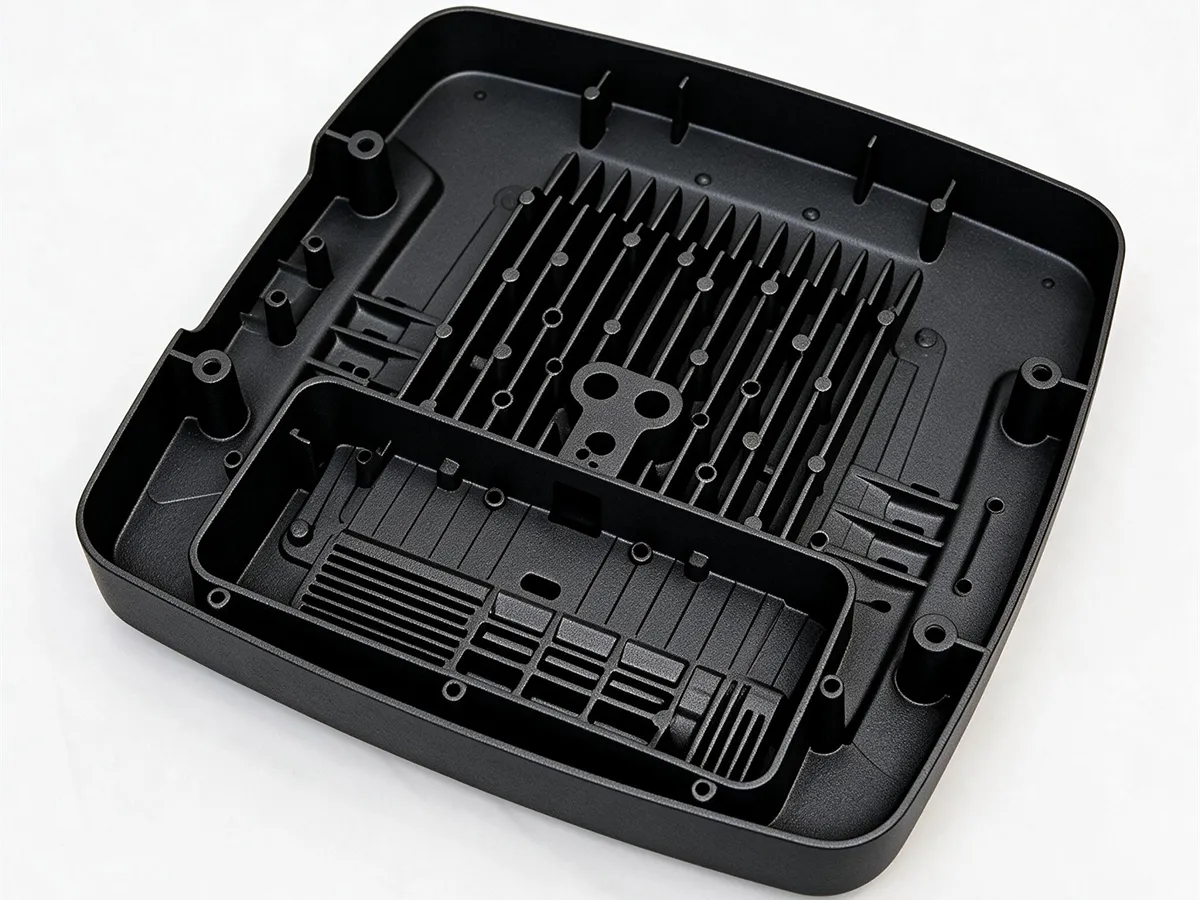
Powder is the default for outdoor hardware, 괄호, and enclosures where color consistency across batches matters more than metallic look. Modern polyester powders carry architectural-grade weatherability specs, and the film is a mechanical barrier that salt-spray testing quantifies directly, with ASTM B117 hours on the pull report. It also lets the part’s appearance be specified independently of its alloy. The same housing comes in ADC12 or A360 with an identical finish, something the anodize route cannot promise on cast material. 그만큼 powder coating guide covers that route in depth.
On the wear side, powder’s weakness is edge coverage, since corners pull thin films and chip first. Its strength is dent and scratch absorption, because the polymer layer has thickness to flex. For hardware that travels, gets torqued down, and lives outside, that trade is usually the one you want.
When Anodizing Keeps the Metallic Look
Anodizing earns its place when the part must keep its metal identity and its dimensions. Hardcoat, the Type III class, delivers the abrasion resistance of a ceramic layer while adding only tens of microns. It keeps tight tolerance chains intact, and it cannot peel because it is not a film, a decisive property for parts in repeated assembly cycles. 그만큼 anodizing mechanism is why that film bonds to the substrate rather than sitting on it. 그만큼 Type II and Type III comparison sets out where each class pays. The metallic look, whether natural gray or the restrained black castings take well, is also hard to fake: coated metal looks coated.
The caveats belong in the spec, not in a surprise at inspection. Expect color mottling on high-silicon alloys, a narrower palette than polymer coatings, and sealed-film sensitivity to strongly alkaline cleaners. There is also an electrical reality: aluminum oxide is an insulator, so grounding and bonding surfaces need masked areas if the housing must carry a circuit path.
The Adjacent Options Buyers Overlook
Real selection is rarely two-way. E-coating deposits a thin, uniform primer-like film that covers internal surfaces powder’s electrostatics cannot reach, used alone for a corrosion barrier or under a powder topcoat for scribe-free edges. See how e-coating compares for castings. Blast pre-treatment before either finish changes the outcome, since it improves powder adhesion and gives anodize a more uniform matte. And plain chemical conversion coatings sit at the economy end when the goal is corrosion protection before shipment rather than a final appearance. Our write-up on trivalent passivation covers that middle ground.
Five Questions That Decide the Finish
1. Does the part need color or the look of metal? Color across batches means powder. Metallic identity means anodize, accepting cast-alloy mottling.
2. Are there fits, 스레드, or grounding surfaces? Tight mating geometry or electrical paths favor anodize, or powder with masking drawn in from the start.
3. What does the part survive outside? Long-term UV and stone-chip duty on structural hardware point to a UV-rated powder system with salt-spray data behind it.
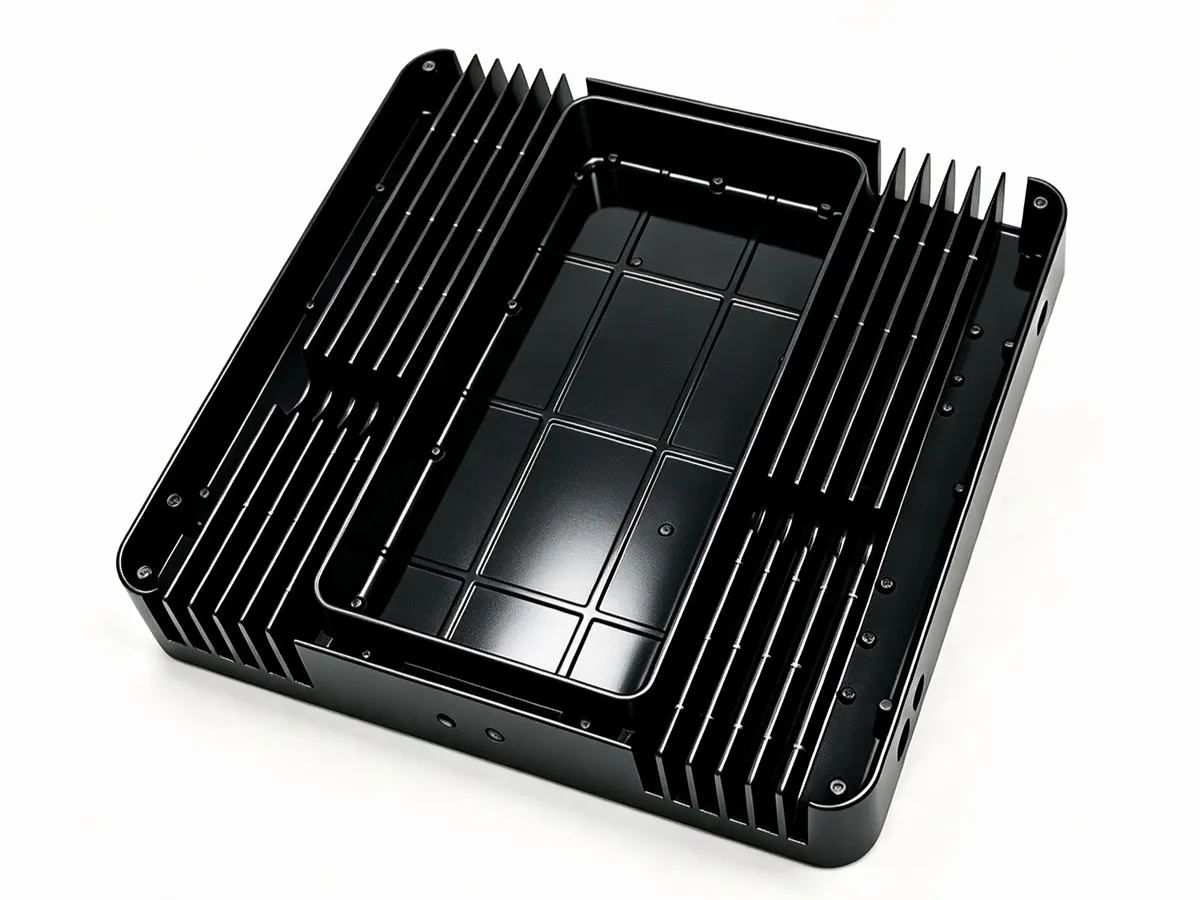
4. How honest is the casting surface? Visible flow lines and porosity paths are broadcast by anodize and bridged by powder, so the question doubles as a DFM check on the die.
5. What will the drawing actually specify? “양극산화처리, black” invites arguments at inspection. “MIL-A-8625 Type II, Class 2, black, 봉인된” 또는 “AAMA-class polyester powder, 60-80 미크론, ASTM B117 tested to specified hours, mask all machined bores” gets you the finish.
Anodizing vs Powder Coating in Production
How a supplier delivers each finish shapes lead time and lot logistics as much as the chemistry does. Bian Diecast runs powder coating in-house on dedicated lines, with salt-spray chambers, color meters, and film-thickness gauges doing the verifying, plus in-house sand and shot blasting as pre-treatment. Anodizing and e-coating go to qualified partner facilities, the normal arrangement for die casters of our size. That adds a transport leg and lot coordination, and it means the color-mottling conversation happens with samples before volume, not after. 그만큼 finishing service category lists the treatments we deliver routinely.
The finishing decision is cheapest to make at DFM stage, when masking callouts and pre-treatment blast can ride along with the die design. Where the casting itself is the variable, the levers stay in our building, from vacuum-assisted processes for denser skins to blast media control before the bath. When two finishes both look viable on the drawing, 통해 보내주세요 연락처 페이지 and the comparison comes back with real sample parts and the cost delta between them.
최종 생각
The anodizing vs powder coating choice is settled by function, not by preference. Anodize keeps the metal identity and the dimensions of a casting, and it tells the truth about the surface underneath. Powder buys color, hiding power, and a thicker corrosion barrier, and it forgives a die-cast skin that anodize would expose. Decide which failure you are protecting against, then specify the finish in the same detail, on samples from your own alloy.
Common Questions About the Two Finishes
Can ADC12 die castings be anodized?
예, and they should be expected to look like it. ADC12’s roughly 10 에게 12 percent silicon stays inert in the bath, so the finish comes back gray and lightly mottled rather than clear color. Functional protection is real; batch-to-batch color is not. In the anodizing vs powder coating decision, anodizing is the functional choice on cast aluminum and powder is the cosmetic one.
Does powder coating change part dimensions?
예. A normal powder build adds roughly 60 에게 120 microns per coated surface. Slip fits, 스레드, pilot diameters, and grounding pads need masking or tolerance allowance drawn in before coating. Anodizing at 5 에게 25 microns in Type II is usually dimensionally forgiving by comparison.
Which finish resists corrosion better outdoors?
As a barrier, a properly applied 60-micron or thicker powder film outperforms a standard Type II anodize layer, because it is thicker and continuous. That is why outdoor hardware specs lean on powder with ASTM B117 salt-spray hours on the report. Sealed anodize holds its own chemically and does not delaminate, and hardcoat raises the wear bar.
Which is cheaper for volume production?
Per part at volume, in-house powder usually wins on throughput and scrap tolerance. Anodizing cost swings with rack density, sealing steps, and whether the finisher is a subcontracted operation that adds logistics to every lot. The larger cost lever is choosing wrong, since re-coating masked threads or rejecting mottled anodize costs more than either finish.