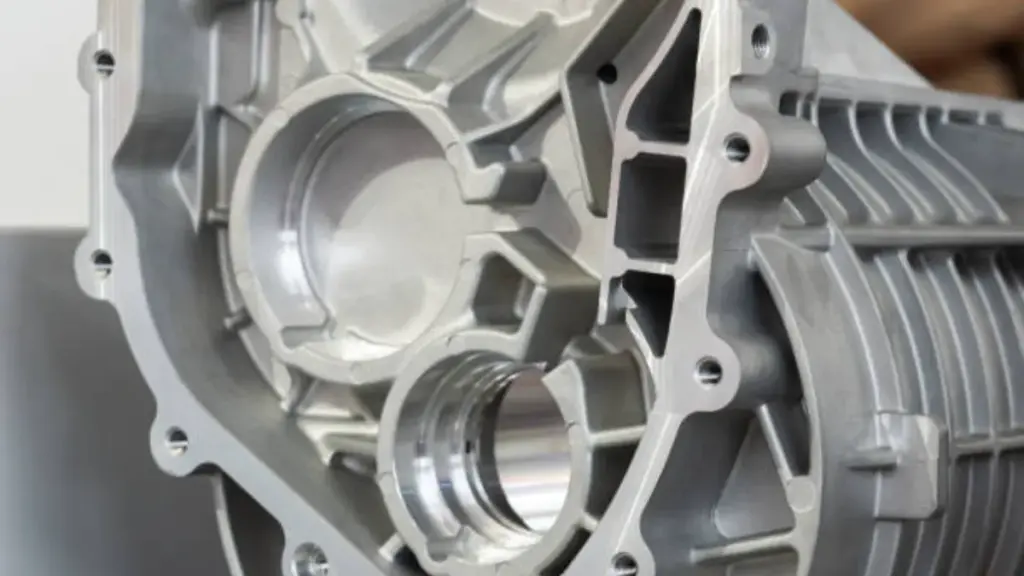
Drop a rack of ADC12 housings into a sulfuric acid bath and a meaningful share of the surface stays inert. The silicon, 9.6 к 12.0 percent of the alloy by weight, does not convert while the aluminum around it turns to oxide. The finish that leaves the sealing tank is gray, frosted, and patterned with the alloy’s own microstructure.
This is not a process failure. It is the default result of anodizing a high-silicon die cast alloy, and the teams who understand it before quoting avoid the most expensive finishing dispute in cast aluminum. This guide covers why the bath resists these alloys, how porosity turns cosmetics into a leak risk, and which countermeasures hold in production.
Why High-Silicon Alloys Fight the Bath
Anodizing grows aluminum oxide out of aluminum. Nothing in that electrochemistry converts primary or eutectic silicon cells, intermetallic particles, or the porosity voids in a high-pressure die cast skin. Three consequences follow, and all three are visible on the part.
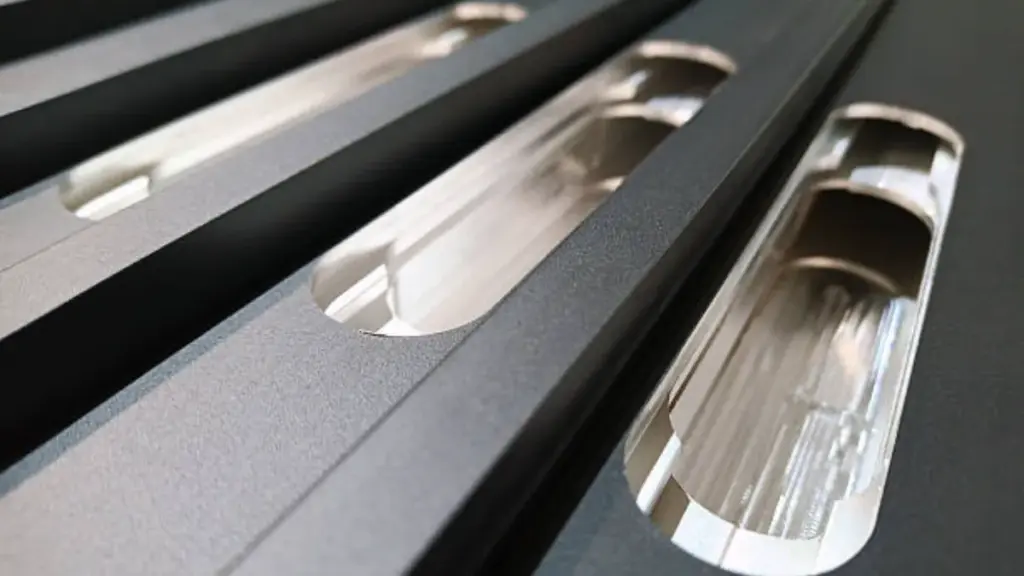
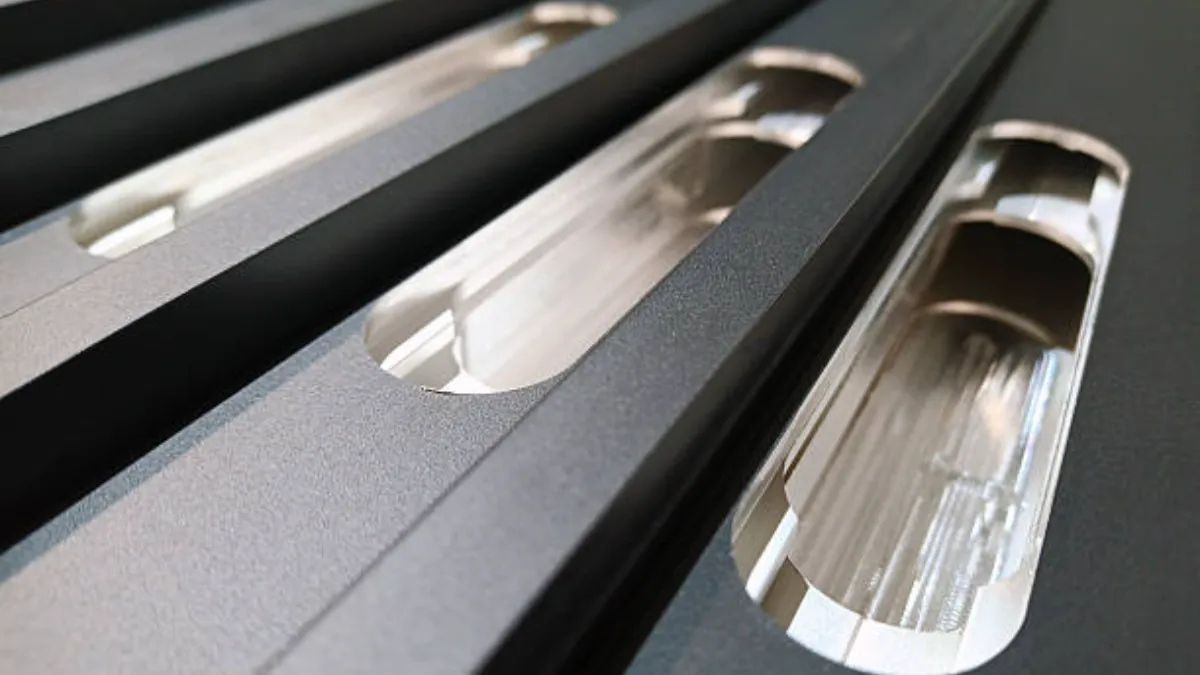
Color and texture. The unreacted silicon sits at the surface as a fine gray pattern once the surrounding film turns translucent and matte. The higher the silicon, the stronger the mottling. Near-eutectic grades such as YL102 (10.0-13.0% И) and ADC1 (11.0-13.0% И) come back the flattest and frostiest. А380 (7.5-9.5% И) sits a little better, though its 3.0-4.0% copper adds its own dark, uneven tint.
Dye inconsistency. MIL-A-8625 anticipates this in plain language: dyed castings may show slight color inconsistency, and the acceptable degree is set by the purchaser, not the anodizer. A color standard approved on a wrought 6061 sample is a promise a die casting cannot keep. For the standard classes behind that note, see the guide to Type II and Type III hard coat.
Die-soldering aftermath. Alloy silicon also attacks tool steel over a die’s life. As cavity wear creeps in, линии потока, холодно закрывается, and micro-welding marks deepen on the casting. Anodize is a conversion coating rather than a build coating, so it reveals each of those marks instead of bridging over them the way powder would. The oxide-growth mechanism explains why a converted film tracks the substrate rather than hiding it.
When Porosity Turns Into a Leak Story
High-pressure die casting traps gas, и process overview documents how that entrainment happens. Fine as the pores are, they connect to the surface after machining, бурение, or through the open channels in the casting skin. That shifts the conversation from cosmetics to reliability.
Acid from the sulfuric bath enters the pores and is not fully neutralized or rinsed out. Hours or days later, especially through hot-water sealing, the trapped acid migrates back out as white bloom, staining, or brownish bleed-out at machined edges. The failure is worst where it is most visible: drilled holes, machined pilot faces, and thread runs, anywhere bare metal was exposed after casting and hits the bath directly.
If a part must pass a leak test later, anodized porosity paths can also host corrosion initiation under the film. That is why pressure-tight housings are a place where finishing sequence and sealing discipline genuinely matter.
The Casting Sends Its Resume Through the Coating
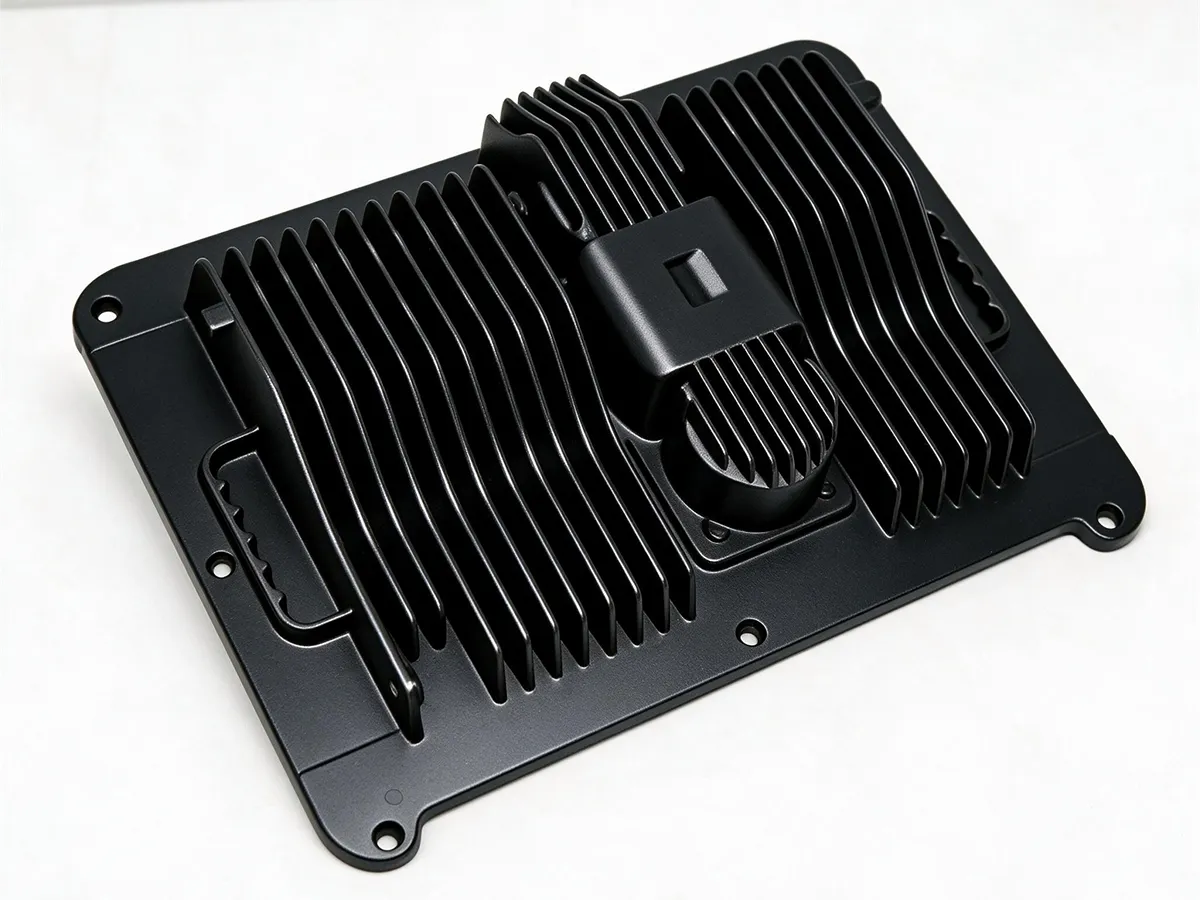
Anodize is honest to a fault. Flow lines from the gate, witness marks from the ejector pin, and the difference between skin and heartmetal where a boss got machined all read on the finished part. Buyers who choose an anodized finish for a clean metal look on cast parts usually find this at first-article review, when the shot pebbles the die had hidden.
Shot and sand blasting before the bath is the standard mitigator. A uniform blast texture scatters light the same way everywhere, dyes take it consistently, and the perceived mottling drops sharply. It is also a two-edged tool. Media that is too coarse digs craters the film then outlines. Fine media, consistent coverage, and the same blast on every batch are the discipline that makes gray-on-gray look intentional.
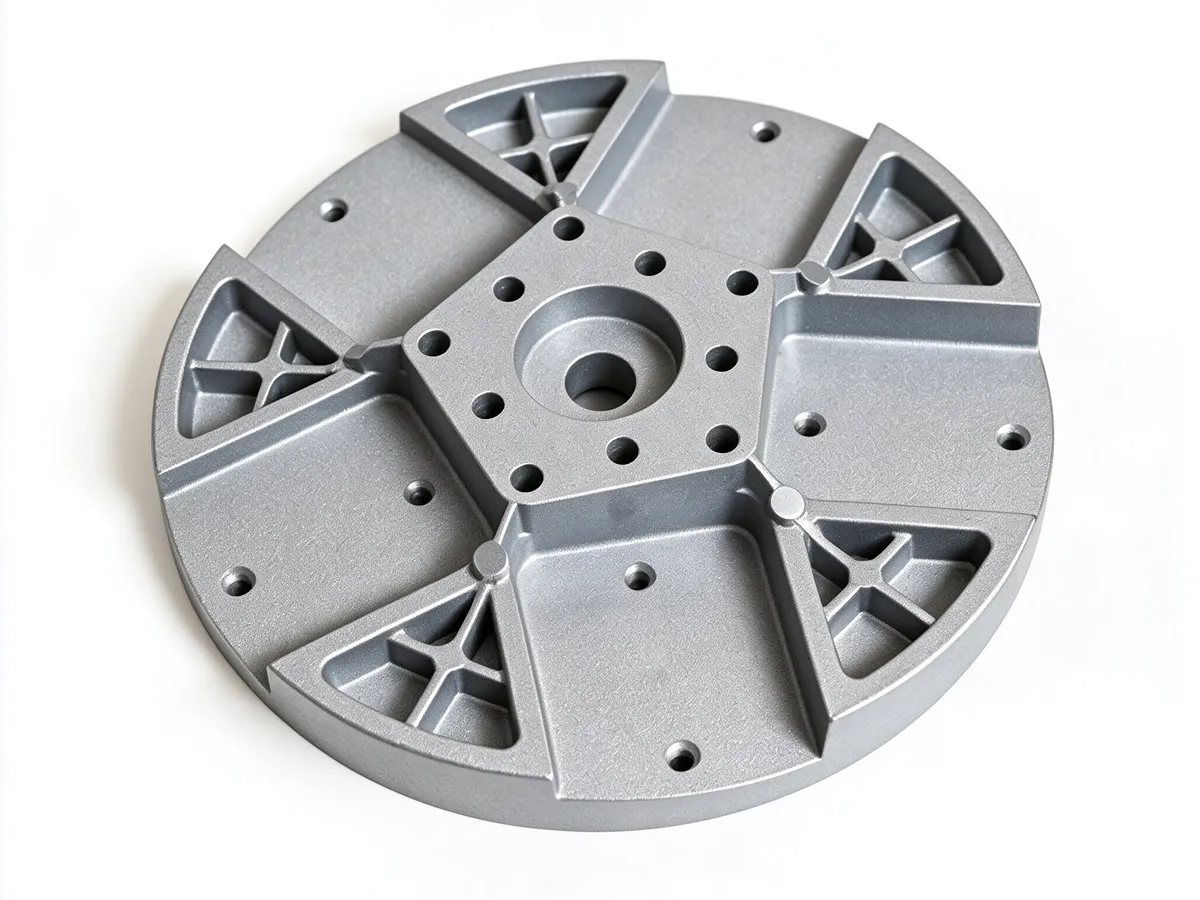
Choosing a Stock Alloy for the Bath
The table reads as a decision fork, not a wish list. Standard grades exist because silicon makes the alloy die-castable: thin walls fill, shrinkage feeding improves, and hot tearing drops. Those composition bands are published values (АСТМ Б85, ДЖИС H5302, ГБ/Т 15115), not vendor folklore. The ADC12 supply guide covers the workhorse high-silicon grade in detail.
| Сплав | Silicon band | Other factors | Anodize outlook |
|---|---|---|---|
| А380 | 7.5-9.5% | Cu 3.0-4.0% | Best of the common grades; dark copper tint |
| АЦП12 | 9.6-12.0% | Cu 1.5-3.5% | Gray mottled matte; functional only |
| А360 | 9.0-10.0% | мг 0.4-0.6%, low Cu | Cleaner gray, better corrosion behavior |
| YL102 / ЛМ6 / АЦП1 | 10.0-13.0% | Cu held low | Frosty, uniform matte; no color claims |
| 518 (special order) | Under 0.35% | мг 7.5-8.5% Al-Mg system | The genuinely anodizable cast grade; costs flow and machinability |
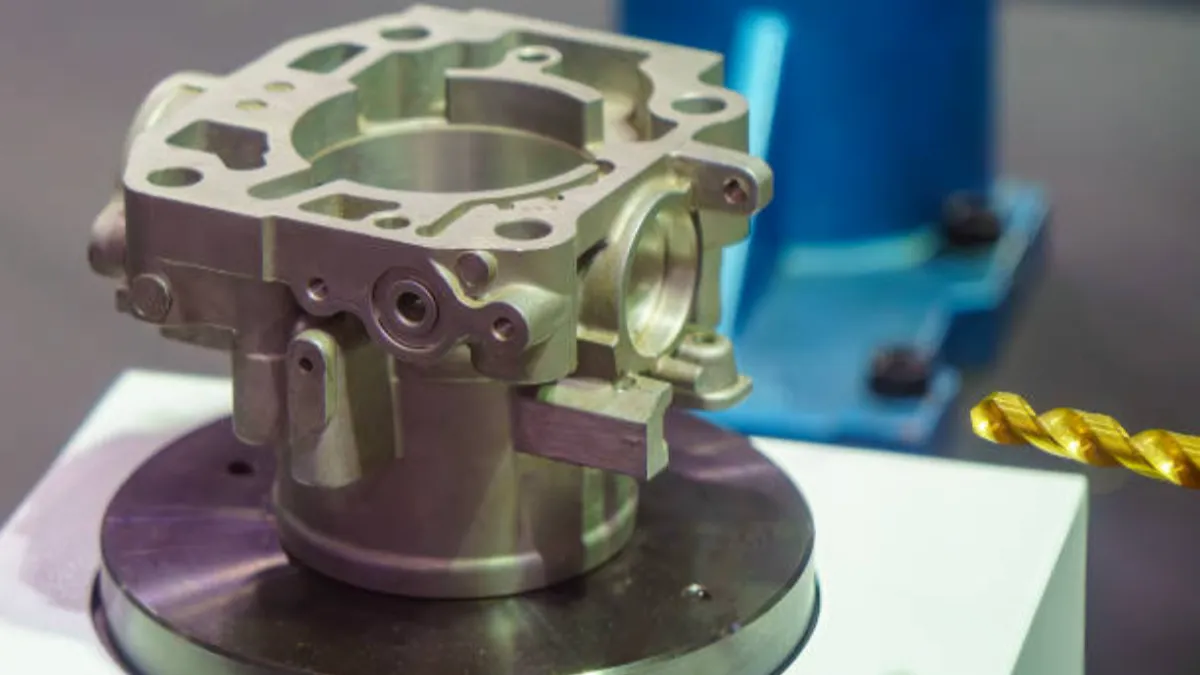
Process Countermeasures That Actually Help
Sealing choice is acid management. Hot-water sealing of porous cast skins is exactly where trapped-bath bleed-out appears. Nickel acetate or dichromate sealing locks the film chemistry down and is the traditional answer on parts that see humid service. Ask which seal the anodizer runs on cast work, and ask to see it on the pull report.
Rinse and neutralize discipline. De-ionized final rinses and a neutralizing step between bath and seal matter most. So do drained racks at machined features, which separate a clean lot from a blooming one six weeks later in a sea container.
Specify Class 1 clear on cast. Dye on a mottled substrate doubles the visual complaint rate for no added protection. Natural, undyed, sealed Type II on a blasted casting is the finish that ages gracefully. If color is mandatory, that is the signal to leave the anodize route and move into coating territory.
Design the finish into the part, not onto it. Grounding pads, thermal interface faces, and press-fit bores can be drawn as masked or as-machined-after-anodize features from the start. Then the coating does not land where it will be scraped or where it can hold acid.
When the Right Answer Is Not Anodizing
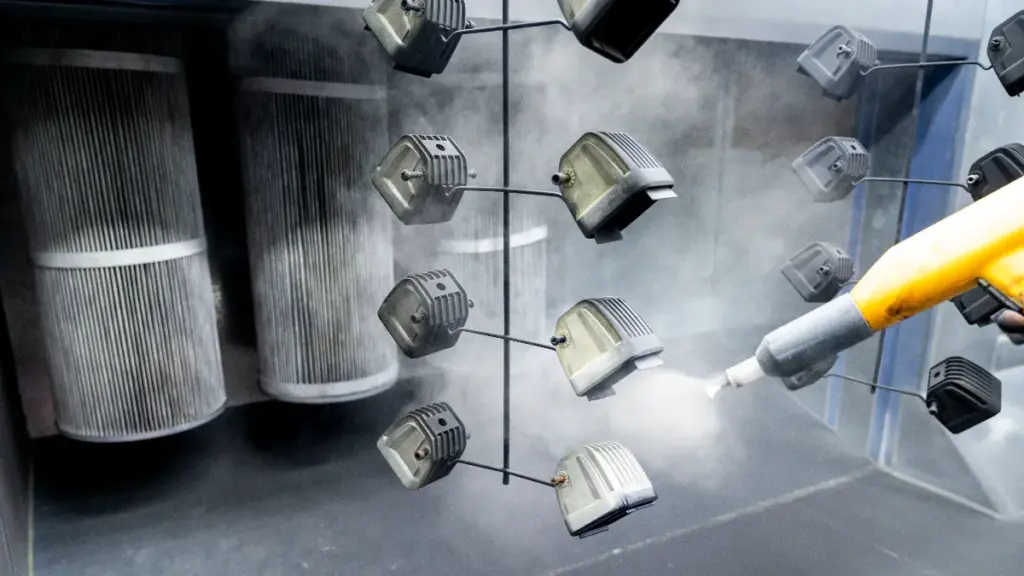
If the real requirement is color, batch uniformity, or hiding power over cast surface variation, an applied coating usually beats a converted one. Polyester powder at 60-120 microns bridges light defects, takes any RAL, and carries UV-rated chemistry with salt-spray hours (АСТМ Б117) on the report. The powder coating guide охватывает этот маршрут.
E-coating lays a thin, cover-uniform film over internal cavities that powder’s electrostatics cannot reach, and it works as a primer under powder for scribe-free edges. See how e-coating compares for castings. A third route is less known. Trivalent conversion coatings give a corrosion base on cast aluminum with the metallic look mostly intact. They sit between bare and anodized in both cost and appearance. Our write-up on trivalent versus chromium-free passivation breaks down what each chemistry does to a casting’s look and shelf life.
What to Settle Before You Commit a Lot
Decide the appearance question on samples from your own alloy and gate location, not on a wrought reference panel. Confirm the seal chemistry and the rinse sequence the anodizer runs on cast work, since those set the bleed-out risk. Ask which finishing steps run in-house and which are managed through partners, and hold the answers to the same gates either way.
Bian Diecast documents its inspection stack on the quality-control service page: direct-reading spectrometry for composition, CMM for dimensions, Рентгенограмма внутренней пористости, and helium leak and cleanliness testing. The finishing service category shows which surface treatments ship with the castings. A finished-part drawing sent through the страница контактов returns an honest routing answer before any volume lot is committed.
Заключительные мысли
High-silicon die cast alloys are not broken parts waiting for a better bath. They are a different material reality, where silicon stays put and the film tells the truth about the casting. Buyers who set appearance on samples and control porosity through sealing and rinse discipline avoid most of the pain. Routing to an applied coating when color is the requirement settles the rest, and keeps cast aluminum from becoming a reputation problem.
Questions About Anodizing High-Silicon Castings
Why does anodized die cast aluminum look gray and mottled?
Because the alloy’s silicon, 7.5-12% in grades like A380 and ADC12, does not convert to oxide in the bath. The inert silicon cells stay metallic while the aluminum around them turns to translucent oxide, producing a frosted, patterned gray. Uniform blasting before the bath makes the pattern consistent rather than distracting.
Can you color match anodizing on a die casting?
Not reliably. MIL-A-8625 notes that dyed castings may show slight color inconsistency and leaves acceptance to the purchaser. Black anodize on blasted castings comes closest. Exact color across batches means powder coating or e-coating instead, where the film is applied rather than converted.
What causes white staining after anodizing cast parts?
Trapped bath acid working out of casting porosity. HPDC gas pores and machined features absorb sulfuric electrolyte, and hot-water sealing drives it back to the surface as bloom or bleed-out. Neutralizing rinses, nickel acetate or dichromate sealing, and drained racking at holes are the standard countermeasures.
Which die casting alloy anodizes best?
Among standard grades, А380 (7.5-9.5% И) gives the least-bad result and A360 the cleanest gray. The genuinely bright anodizers are low-silicon cast grades like 518, под 0.35% И, but they are harder to die cast. They fill thinner walls with more trouble, tear hot, and wear the die faster. Choose the alloy for the part first, then set appearance expectations from samples.