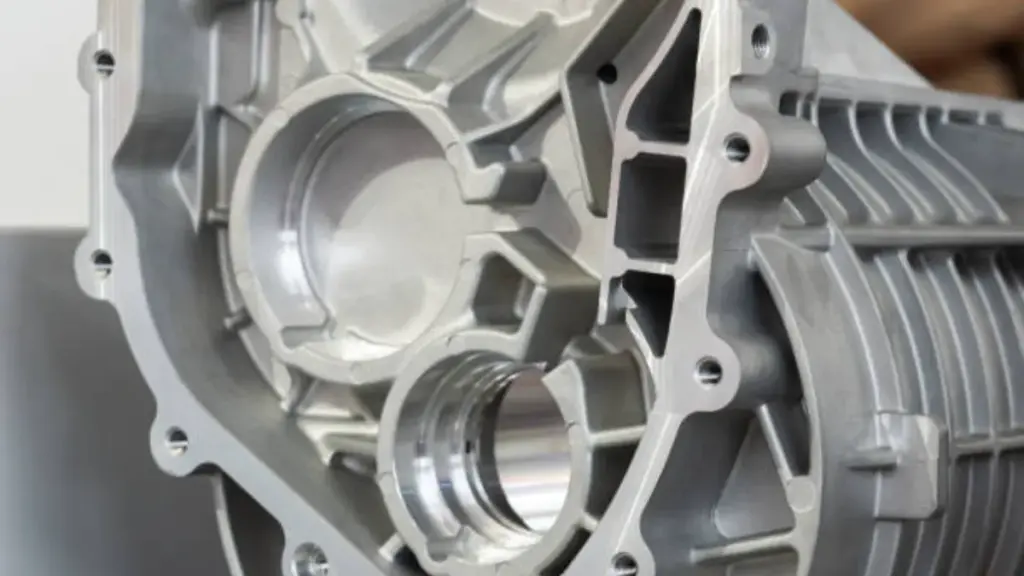
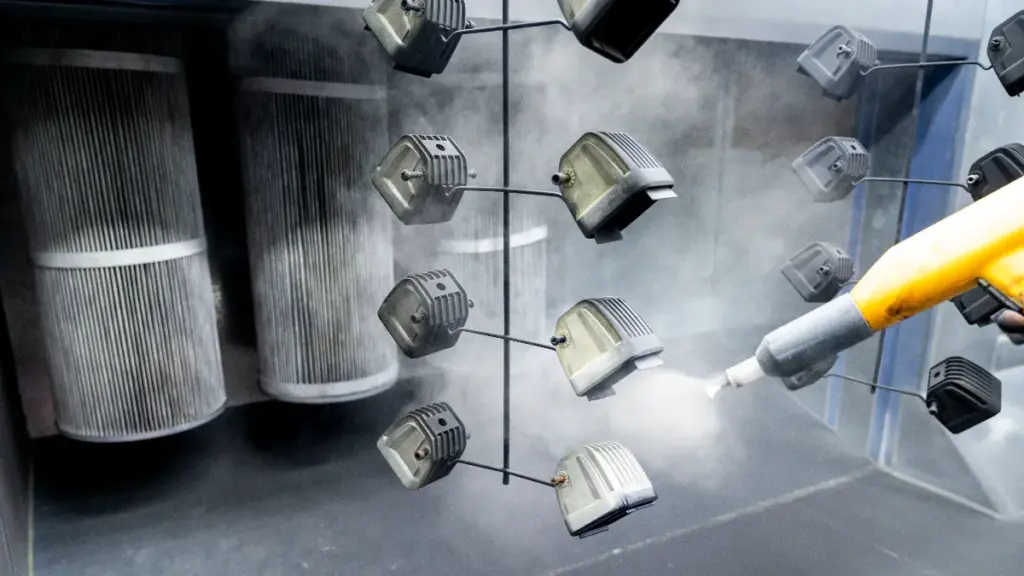
Every custom alloy business case dies in the same place. The spreadsheet compares one metal price to another and crowns the standard grade. That is the wrong comparison. The cost of “use ADC12 and make it work” is not on the ingot quote. It is the extra machining pass, the thicker wall, the leak-test reject bucket, and the field claim. The cost of special metal is not the chemistry either. It is a program with one-time gates that either amortize at your volume or they do not. For high-volume buyers the real question is which side of that amortization line the part sits on. The honest answer moves with annual pieces more than with any other input in the model.
What the Standard Grade Actually Costs
Standard die-casting alloys are cheap in one obvious way and expensive in ways that only appear downstream. Open-market ingot, published bands, and decades of foundry familiarity. Pick the nearest stock grade for a part that needs more heat flow, more pressure tightness, or more hot strength than that grade can honestly deliver. The workaround cost then lands in the operations budget instead of the material budget.
The tax shows up as walls thickened to survive a thermal duty the metal cannot carry, which adds weight, 사이클 시간, and shrinkage risk. It shows up as machining time added to hit flatness the casting warps away. It shows up as coating added to close corrosion margins, and as scrap bucketed because the alloy will not fill the geometry cleanly. None of it is on the bill of materials. All of it is real cost per piece.
Die casting earns its place in manufacturing. It makes complex geometry at high volume and at a low cost per piece, as the ScienceDirect overview of the process puts it. At that volume the per-piece tax compounds, which is the same arithmetic the die-casting cost breakdown walks through line by line.
Before any special-metal conversation starts, pull the last twelve months of rejects, rework hours, down-gauging attempts, warranty credits, and engineering change orders tied to material limits. That figure is the do-nothing baseline, and buyers usually remember it badly.
Where the Custom Alloy Money Goes
The custom side splits into two categories with opposite math, and mixing them is how business cases get misread.
One-time program costs. Development labor on both sides of the table, the trial heats, and the trial shots come first. The qualification package follows: spectrometer verification per heat, metallographic confirmation, mechanical coupons, and X-ray plus leak studies on the new metal. Add any tooling change the trial reveals. These are real but bounded, and they are the part a high-volume buyer can amortize. Ask for an itemized quote so each gate stays visible, and ask whether tooling can be refunded or offset against agreed cumulative volume.
Recurring per-piece costs. Non-standard ingot carries supplier minimums and longer material lead times. Special chemistry can run harsher on tooling, since die soldering and wear are the classic copper-and-iron arguments. Changeover discipline is tighter because the wrong bin cannot be grabbed. These do not amortize. They ride on every casting forever, which is why the custom alloy case is won or lost on the per-piece delta between the two routes, not on the development fee.
The Full Cost Ledger Line by Line
Run every row at your real volume before deciding. The table below is the whole argument in one view.
| Cost line | Standard grade pushed past its limits | Fit-for-duty custom alloy | How to measure it |
|---|---|---|---|
| 재료 | Open-market ingot price | Ingot plus program premium | Supplier quote per kg, both routes |
| Foundry yield | Fill and shrinkage rejects, re-melt losses | Trial-proven yield band | Scrap rate over ten production lots |
| Downstream work | Extra machining, straightening, coating passes | Near-zero if the alloy does the job as-cast | Cycle minutes and operations per part |
| Tooling life | Known wear behavior | Measured during trials, the honest unknown | Die-soldering interval, re-grind frequency |
| Field exposure | Warranty on thermal, leak, or corrosion margins | Margin moved into the metal | Claims per million pieces, last twelve months |
On a 10,000-piece program the one-time costs dominate and the standard grade usually wins. On a 3-million-piece annual part the one-time column shrinks to fractions of a cent per piece, and the recurring rows, 생산하다, downstream work, and field exposure, become the whole argument. The same alloy decision genuinely has different right answers at different volumes. A buyer who has not computed their crossover point is guessing.
Which Property Walls Turn Into Money
Not every property gap is worth program money. Four walls convert reliably at volume, and they explain most of the special-metal programs a die caster sees. 그만큼 alloy selection guide covers the metallurgy behind each trade-off.
Thermal flow. The clearest one in the LED and power-housing world. Standard copper-tolerant die-casting alloys sit in a narrow band of thermal conductivity, while purpose-built high-conductivity grades push well above that band. The payoff is part consolidation plus lumen-maintenance warranty exposure, because the housing carries heat that a bolted-on heat sink otherwise has to remove. The property basis is summarized in the ScienceDirect overview of aluminum alloys.
압력 견고성. For housings that must hold a leak test, automotive fluid paths and sealed electrical enclosures, porosity is the recurring tax. An alloy that feeds better at the geometry’s hot spots converts directly into yield. Inspection methods such as X-ray, hydrogen melt testing, and air- or helium-leak testing exist for a reason. The difference between dense and leaky is a per-piece cost at production rate, and it is measurable on trial shots before you commit. 그만큼 porosity guide covers that failure mode in depth.
Machining response. Parts that leave the die for precision CNC carry the alloy’s machining character in their cycle time. Silicon phase, intermetallics, and iron content decide tool wear and achievable feed. A grade trimmed for machinability buys minutes out of every downstream cycle, which at volume dwarfs any ingot premium.
Hot strength. Under-hood and near-heat-source duty pushes buyers toward copper-rich Al-Si-Cu grades for the strength that survives at temperature. The payoff is wall reduction and mass, a real currency in vehicle programs where the cost conversation returns to kilograms.
The Risks That Break the Case
Three failure modes kill more special-metal programs than metallurgy does. 첫 번째, tooling wear found late. A special chemistry that begins to solder to the die tens of thousands of shots in quietly moves the recurring-cost column the wrong way. That is why die-soldering behavior belongs in the trial protocol, not the assumptions. 두번째, requalification drag. Change the alloy on an IATF 16949 program and every downstream paperwork artifact, PPAP, 재료 인증서, and customer-specific requirements, moves with it. Budget the calendar, not just the dollars. 제삼, single-source lock-in. A proprietary or trimmed chemistry can mean one ingot supplier, one price line, and one lead time you now own the risk of. 묻다, 서면으로, who else can pour your composition before you sign.
None of these are reasons to refuse a custom alloy. They are the three columns the ROI sheet needs that buyers keep leaving blank.
Structuring the Deal so the Math Survives
The commercial architecture matters as much as the spreadsheet. Four terms keep the special-metal case honest through negotiation. One: stage the gates, a property-target sheet, then trial shots with full reports, then a priced production pilot, with a stop decision owned at each gate. A program that cannot stop cheaply early rarely stops. Two: demand the itemized cost ledger from the first quote, 금속, 프로세스, 마무리 손질, and tooling each separable, because volume discounts on a bundle are how per-piece truth gets hidden. Three: tie any tooling refund to realistic cumulative volume, 서면으로, since that refund is the mechanism that converts the one-time column into an amortization schedule. Four: put the MOQ ladder into the model. Special metal stacks supplier minimums on top of standard-grade minimums, and a business case computed at trial-lot quantities is fiction at production quantities.
A foundry that runs MES-tracked production, per-heat spectrometer control on a central melting furnace, and ships raw-material test reports with each lot is not selling you a cost line. That is the verification infrastructure that makes the ROI numbers defensible, and it is what the capability list describes end to end.
최종 생각
At low volume, buy the standard grade and engineer around it, because the one-time costs have no base to amortize against. At genuine high volume, stop comparing metal prices and compare total per-piece cost, including everything the workaround tax hides: 생산하다, downstream operations, warranty, and the requalification calendar. Ask whether the property wall is one of the four that converts: 열의, tightness, 가공, or hot strength. If it is, and the ledger above comes out positive at your real annual pieces, the custom alloy is a capital decision with a measurable payback. 그렇지 않은 경우, the standard menu already contains your answer. Bring the volume, the wall, and the twelve-month reject data to the 연락처 페이지 and the crossover question gets answered with arithmetic instead of adjectives.
Questions Buyers Ask About Alloy ROI
Is a custom alloy cheaper than ADC12 at high volume?
킬로그램당, no, because special metal carries a program premium over open-market ingot. Per finished part it can be, once you add what the standard grade costs downstream: yield loss, extra machining, thicker walls, coating compensation, and warranty exposure. The decision is total per-piece cost at your annual volume, not the material line.
What volume does a custom alloy program need to pay back?
Compute the crossover: one-time program cost divided by annual pieces must be smaller than the per-piece delta the alloy saves. A mid-five-figure program against a 3-million-piece annual part amortizes to well under a cent each, while the same program on 50,000 pieces does not surface. Tooling-refund thresholds tied to cumulative volume are the standard mechanism for making that math work for both sides.
What recurring costs come with a non-standard alloy?
Three do not amortize. The first is ingot program minimums and longer material lead times. The next are tooling-wear and die-soldering behavior measured during trials, and single-source lock-in on a composition only one supplier pours. Put them in the ledger before the business case gets signed, because they ride on every piece forever.
Does changing alloy affect automotive qualification?
예. On an IATF 16949 program the material change moves the whole paperwork set: PPAP resubmission, per-heat certificates, and customer-specific requirements. The requalification calendar is a real cost in the model, so budget it in weeks as well as dollars. Confirm scope with the end customer before the trial gate closes.