Two die castings arrive at the same drawing number, identical except for one finish callout. One says buff to a mirror. The other says powder coat, RAL 9006. The mirror part spends hours in the polishing shop; the coated part spends minutes on a rack and an oven cycle.
Buyers routinely pay mirror economics for parts that were going to be coated anyway. Others specify a coating over a surface so uneven that the finish fails inspection regardless. The polishing-versus-coating decision is a cost question with an appearance constraint attached. Getting it right means knowing what each process charges for, and what each one can and cannot hide. The basics of specifying a cast surface are covered in this site’s guide to surface finish for die casting parts.
What a Bright Finish Actually Requires
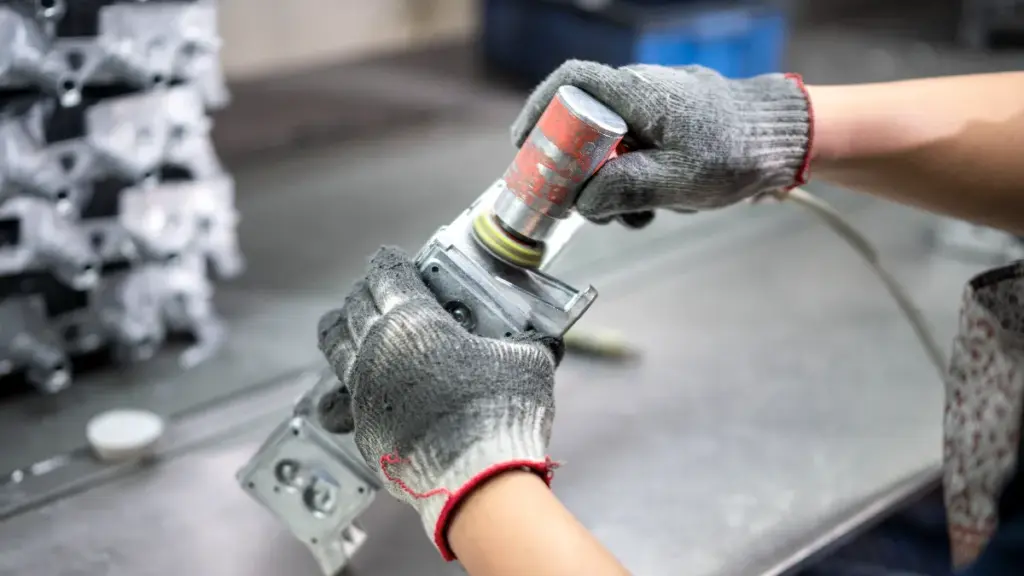
A bright mirror is not a single operation. It is a sequence of progressively finer cutting stages, each one removing the scratches left by the last. A die cast part enters the sequence with flow lines, vent witness marks, and a thin dense skin formed where the melt met cold steel. That skin is what makes a bright finish possible, and it is also what a mirror puts at risk. Buff too hard and the wheel cuts through the skin into the softer, more porous metal underneath, where gas holes and shrinkage cavities appear as pinholes no compound can fill.
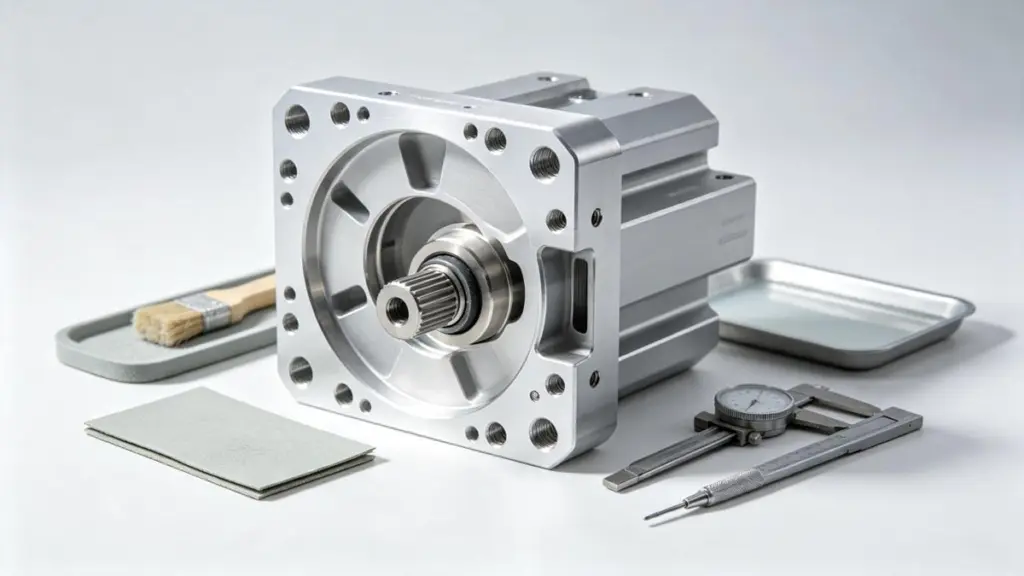
The requirement is therefore two-sided. The casting must be sound enough to survive the cut, and the polishing must be controlled enough not to destroy the geometry the die worked to create. Edge radii round over. Flat faces develop a slight dish. Deep bores and internal corners stay unreachable. A mirror spec on a complex housing often means a bright exterior over a raw interior, a cosmetic compromise the buyer should know about before tooling is cut.
Vibratory and barrel finishing solve some of this by spreading the work across a batch. Parts tumble in media and compound, and the process evens edges and produces a uniform satin sheen at a cost per piece that manual buffing cannot match. It does not produce a true mirror, 그렇지만. Satin and bright are different targets, and the drawing should name which one it wants.
Why the Finish Callout Drives Cost
Polishing and coating are priced by different units, so the callout on the drawing moves the invoice in different directions. A mirror finish is bought by the hand-hour, and it interrogates the casting underneath it. A coating is bought by the square metre, and it forgives the casting underneath it. The rest of this guide turns that asymmetry into a decision a buyer can defend in a quote review.
The Real Cost of Polishing
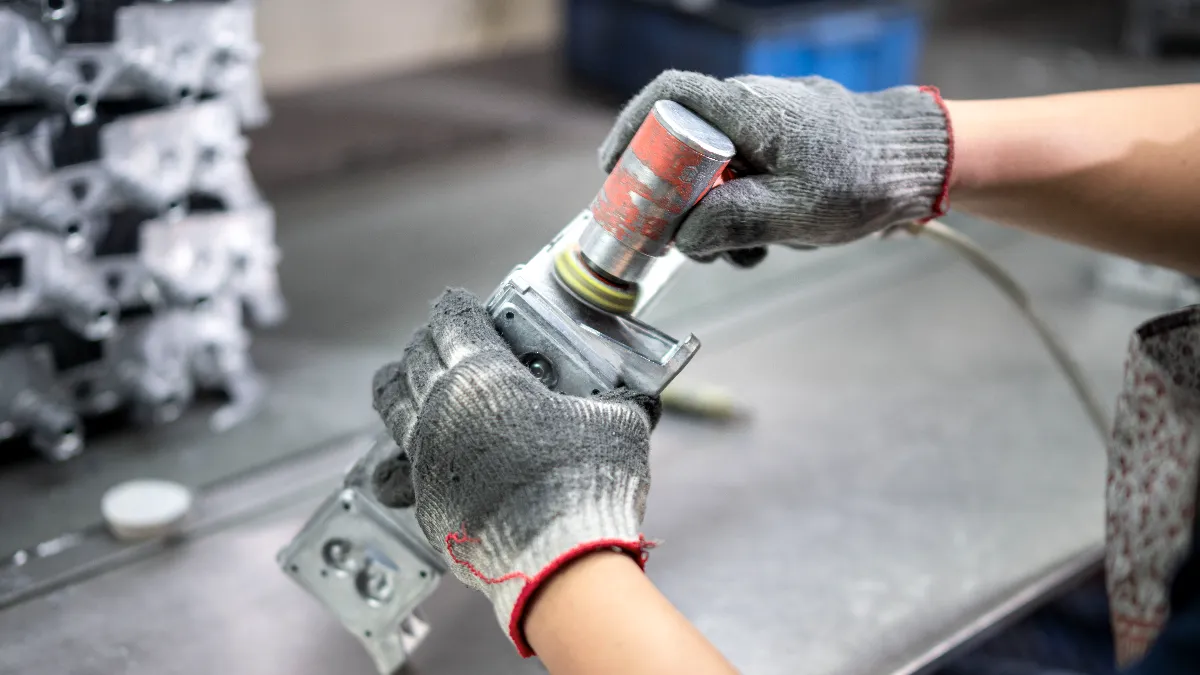
Polishing charges by the piece and by the hand-hour. A buffed finish is built in stages, from a cutting compound that flattens, to finer compounds that brighten, to a coloring wheel that brings the luster. Every brighter grade adds stages, slower wheel time, and more operator attention. The hidden cost is yield. Over-polished edges round over, radii shift, and subsurface porosity appears once the dense die-skin is cut through. A mirror finish quietly buys a casting-quality requirement as well: pinhole-free skin, degassed melt, and tight die maintenance.
Only vibratory finishing scales, because it is batch economics. Media, compound, and cycle hours spread across hundreds of parts in a tub. Mirror-level buffing does not scale that way. It is selective, skill-dependent work on individual parts. The deburring and polishing steps that lead to a bright surface are described on this site’s deburring and polishing page.
The Cost Structure of Coating
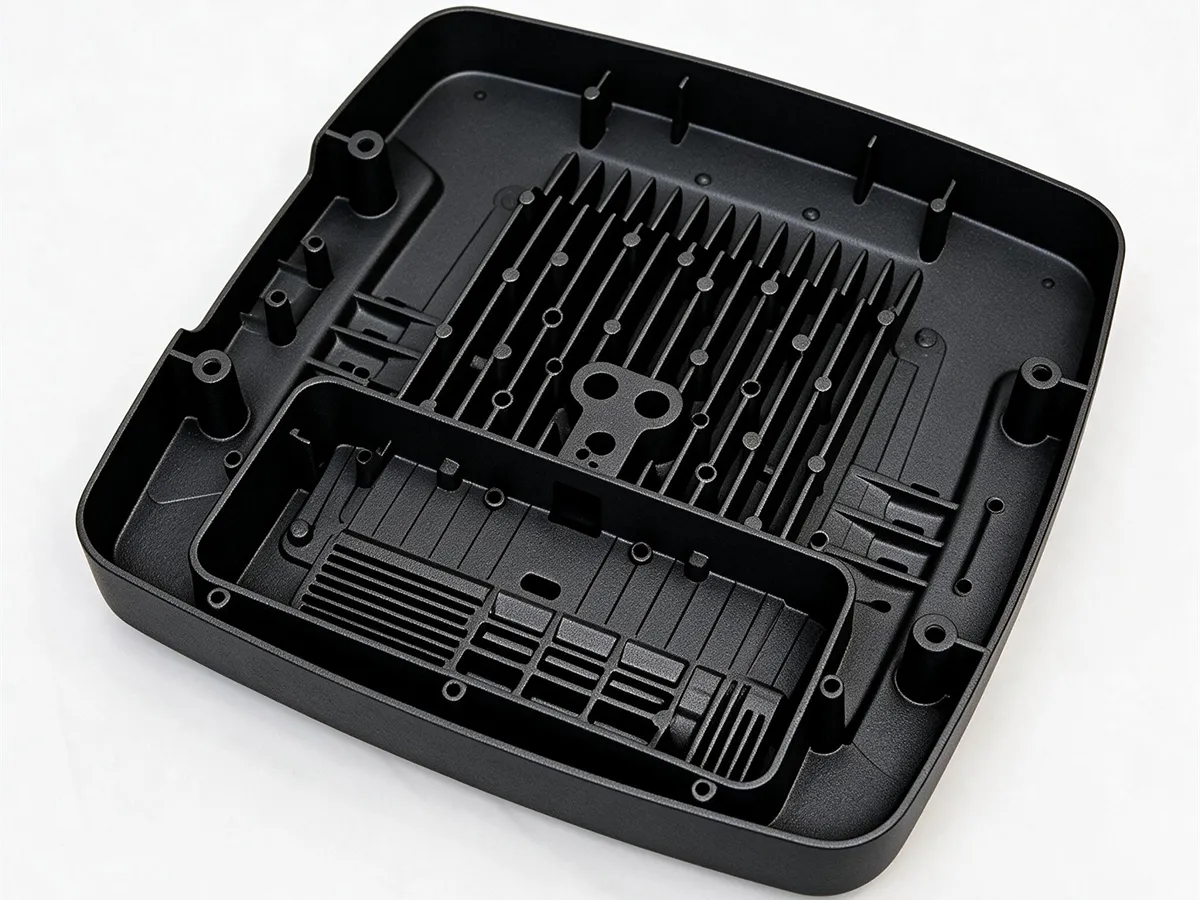
Coating charges by the square metre and the rack, not by the hand. Parts go on fixtures, get a preparation step, receive powder or dip, and cure in a bake line. The preparation is usually a degrease plus a blast that evens the surface and opens the mechanical key the film adheres to. The variables that move the number are pre-treatment grade, film thickness, color changeovers on the powder booth, and masking where a threaded bore or thermal pad must stay bare. The finishing options a shop offers, and how they are grouped, are listed on this site’s finishing service page.
Coating also buys protection. A continuous organic film is the corrosion barrier for outdoor and automotive hardware. Salt-spray performance, run to ASTM B117 or an automotive cyclic equivalent, is engineered through the film system and its preparation, not through the metal underneath.
Bare polished aluminum does none of that protection work. It oxidizes and stains outdoors, so an exterior decorative part often needs a clear lacquer or a clear anodize layer over the polish. ㅏ “polished” outdoor part is frequently a polished-plus-coated part, paying for both processes.
Polishing Versus Coating Side by Side
| 차원 | Polished bare metal | Coated film |
|---|---|---|
| Cost driver | Per-piece labor and stages | Per-area film, prep, and cure |
| Hides casting marks | 아니요, it reveals flow lines and porosity | 예, within film thickness and texture |
| Color options | Metal only, anodize adds tint cost | Any RAL color, 광택, and texture |
| Corrosion path | Needs lacquer or anodize outdoors | The film is the protection |
| Batch consistency | Skill-variable, part to part | Rack-uniform and repeatable |
| Dimensional risk | Rounds edges, can shift dimensions | Film builds on tight fits, mask or spec it |
Read the table as an economic statement. Polishing buys an appearance only bare metal can deliver, and pays labor rates for it. Coating buys appearance, protection, and consistency together at industrial rates. The mistake is paying for the wrong one.
When a Mirror Finish Pays Off
A mirror finish earns its cost in three situations. 첫 번째, the metal feel is the product: 장식 트림, architectural hardware, appliance accents, and reflector surfaces where specular brightness is a functional optical property. 두번째, the surface is touched again and again, as on handles, 손잡이, and fixtures, where a coating would wear through and bare metal ages better than a chipped paint edge. 제삼, a downstream process needs the flatness itself, such as a sealing or thermal-contact face where a coating layer would add thermal resistance or compress under a gasket.
Outside those cases, a mirror is usually the wrong buy. If a coating is going on anyway, a buffed surface underneath is spend that buys nothing. If the casting has no chance of being pinhole-free, the polish interrogates melt quality you may not be buying. And when “polished” on the drawing really meant “clean and smooth,” the same budget goes further as a blast or vibratory prep plus a coating.
When Coating Beats the Polish
Coating wins on cost, 일관성, and protection at once for most exterior and interior hardware. A uniform film hides the flow lines and vent marks that a mirror would expose. It delivers color and gloss across every face on the rack, including the ones nobody would polish. Where the brief is weatherability and color rather than metal luster, a preparation blast plus a powder coat delivers it in a single finished process. This site’s guide to powder coating for aluminum die castings covers the coat systems that preparation depends on.
Once coating wins, the choice between an immersion e-coat and a sprayed powder is a separate decision about film build and geometry. E-coat wraps complex internal channels in a thin, even film; powder builds a thicker, harder, colored coat on exterior faces. That comparison is its own topic, and anodize sits outside both as a converted oxide layer rather than a paint film, described on the anodizing explainer.
How to Specify the Finish on the Drawing
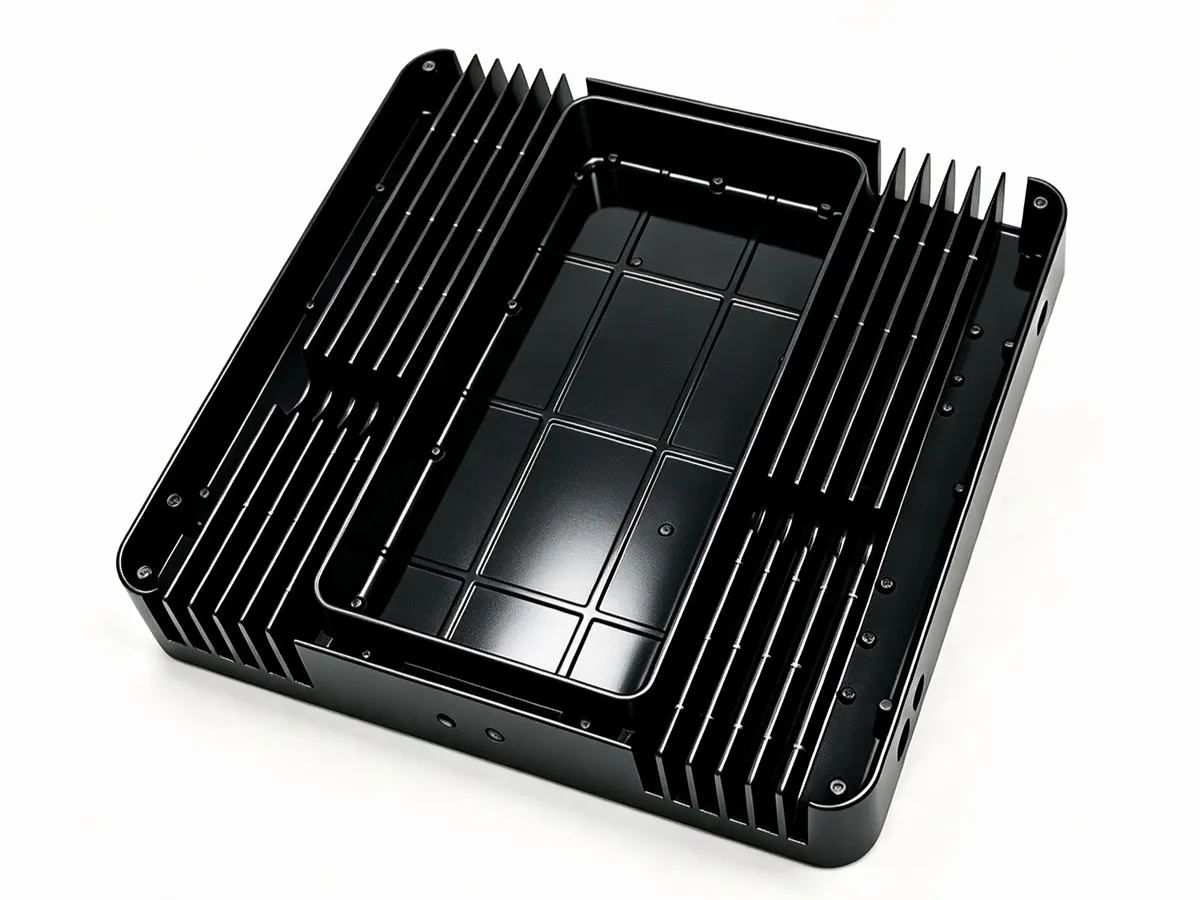
The drawing should state the function the finish serves, not just a process name. A callout that says only “polish” leaves acceptance ambiguous, because smooth is a judgment two inspectors can reach differently. A better callout names what matters for the part: the specular look, a surface texture reference, or the flatness a sealing face needs. Where appearance drives the decision, attach an approved first-article sample or a gloss range so the shop and the buyer judge against the same target.
Then zone the faces. Mark which surfaces are cosmetic, which are hidden, and which are machined mating surfaces that must stay bare and hold their own tolerance. Note where a coating film would interfere with a fit or a thread so those areas get masked or left as-cast. If a mirror is required, state the casting-quality level it depends on, because a bright finish on a porous casting is a promise the process cannot reliably keep.
Zoning the Finish Across the Part
Mature programs rarely pick one process for the whole part; they zone the finish. The visible face gets the bright polish or the premium coating. Hidden and internal faces stay as-cast and deburred. Mating surfaces are machined to their own tolerance and left bare. Under a coating spec, a sandblast stage does more for final appearance than any polish can. It evens the color take and kills flow-line shadowing under the film. Textured powder over a blasted base is the cheapest route to a part that looks flawless.
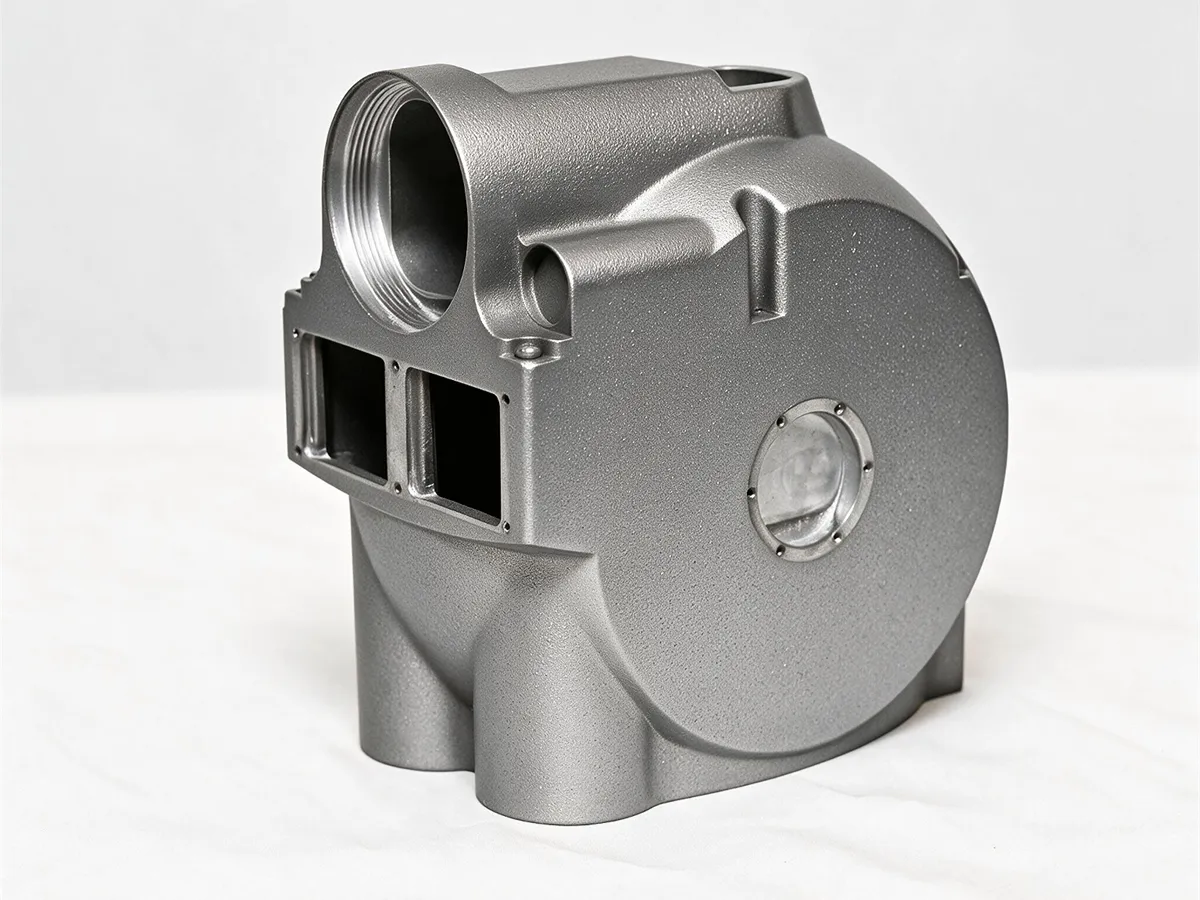
The same zoning logic applies where a bare-metal look is wanted on the outside but corrosion is the real requirement. A clear anodize over a polished cosmetic face, or an e-coat primer under a powder topcoat on an automotive bracket, buys protection without polishing surfaces no one will see. Sequencing these steps against the machining work is covered in this site’s post-machining finishing guide.
Questions About Polishing and Coating
Is polishing cheaper than coating a die casting?
Rarely at production volume. Buffing is per-piece labor through several stages, while a powder coat charges by area on racks with an oven cycle and hides substrate variation. Polishing makes economic sense only when bare-metal appearance or a functional flat surface is the actual requirement.
When should I specify a mirror finish?
Specify a mirror finish when the metal look is the product or when the part is handled often enough to wear a coating through. A sealing or thermal-contact face that needs true flatness also justifies a mirror. If none of those apply, a blast-and-coat route usually reaches the same appearance for far less.
Can a coated part skip surface preparation?
아니요. Preparation decides most coated-part appearance. A sandblast or vibratory stage evens the surface, removes flash and release residue, and opens the mechanical key the film needs. Coating a raw as-cast surface reproduces flow lines and vent marks through the film, and gloss paint shows them even more strongly.
Does a polished outdoor part need a coating too?
Bare polished aluminum oxidizes and stains outdoors, so exterior decorative parts normally add a clear lacquer or clear anodize over the polish, and both processes get quoted. If the brief is color and weatherability rather than metal luster, a preparation blast plus a coating delivers it in one finished process.
최종 생각
The finish callout is a cost decision wearing an appearance label. A mirror buys something only bare metal can give, and it charges hand-hour rates plus a casting-quality premium to do it. A coating buys appearance, protection, and consistency together at industrial rates, and forgives the surface underneath. Specify a mirror finish where the metal is the product or the flatness is functional; reach for a coating everywhere else.
The cheapest way to settle it is to put both prices on one sheet before the tool is cut. Send the model with the cosmetic faces marked, the operating environment, the color requirement, and the annual volume through the 연락처 페이지. Ask for the buffed route and the blast-and-coat route side by side. The quote returns with a free DFM analysis report that states the recommendation in writing.