Ask a foundry for an A319 aluminum alloy program and two very different conversations can follow. One is a sourcing exercise: the grade is published, the ingot exists, and the metal only has to reach your drawing. The other is a development exercise: the drawing came from a sand-casting handbook, and the part was designed for high-pressure die casting. Nobody has admitted that the two processes do not share a language of walls, radii, e tolerâncias. Eight weeks is a realistic spec-to-production plan only if you run it as the second conversation while treating the first as settled.
What the A319 Aluminum Alloy Actually Is
A319 is an Al-Si-Cu casting alloy, designation 319.0 under ASTM B26 and UNS A03190. It sits in the same silicon-copper casting family as the A380 and ADC12 workhorses of the die casting industry, but it is tuned in the opposite direction. Where A380 runs 7.5-9.5% silicon with 3.0-4.0% copper to fill thin walls at high pressure, A319 holds silicon near 5.5-6.5% with a comparable copper load. Magnesium stays deliberately low. The alloy trades raw fluidity for the properties that matter once the part is in service: strength that holds as the casting gets hot, estanqueidade à pressão, and clean machining.
Read those published bands as a menu of consequences rather than a certificate to file. The copper that gives A319 its hot strength also costs corrosion resistance against low-copper alloys and changes how the metal behaves against steel cutting tools. The low silicon that helps machining also means the alloy does not pour like a die-casting grade. That single trade is why A319 foundry practice leans on sand casting, permanent mold, and squeeze casting instead of cold-chamber HPDC lines. O alloy families explained guide covers how the silicon-to-copper balance moves every one of these properties.
| Elemento | Published band | What it buys in service |
|---|---|---|
| Silício | 5.5-6.5% | Fluidity and feeding, held low for strength and machining |
| Cobre | 3.0-4.0% | Hot strength and hardness; the alloy’s signature element |
| Ferro | Max 1.0% | Impurity ceiling; above it, brittle phases hurt machining |
| Magnésio | Max 0.1% | Kept minimal; A319 does not use the Mg2Si response |
| Zinco / Mn / Ni | Max 1.0 / 0.5 / 0.35% | Impurity envelopes; manganese partly offsets the iron phase |
Why Buyers Land on A319 in Practice
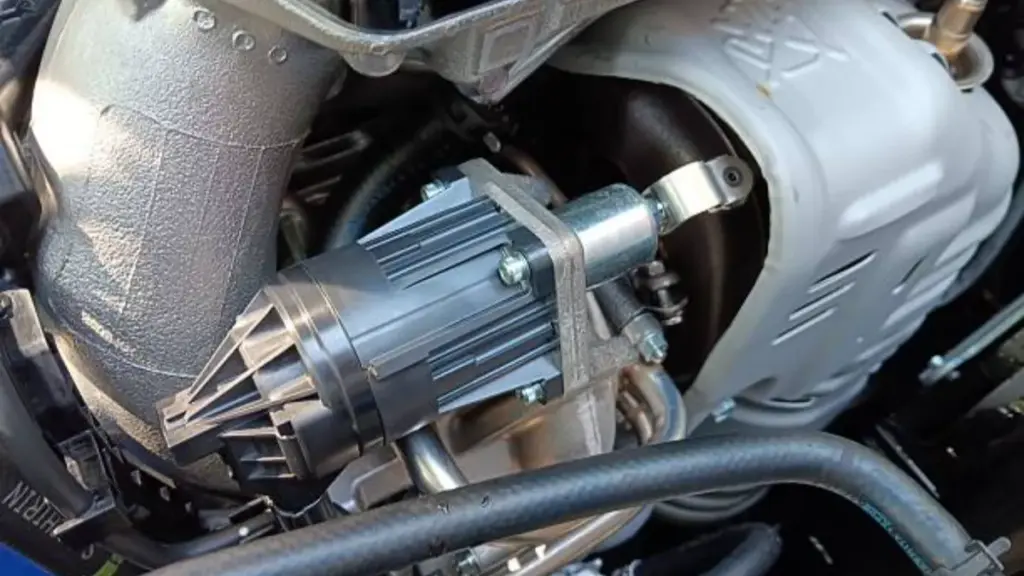
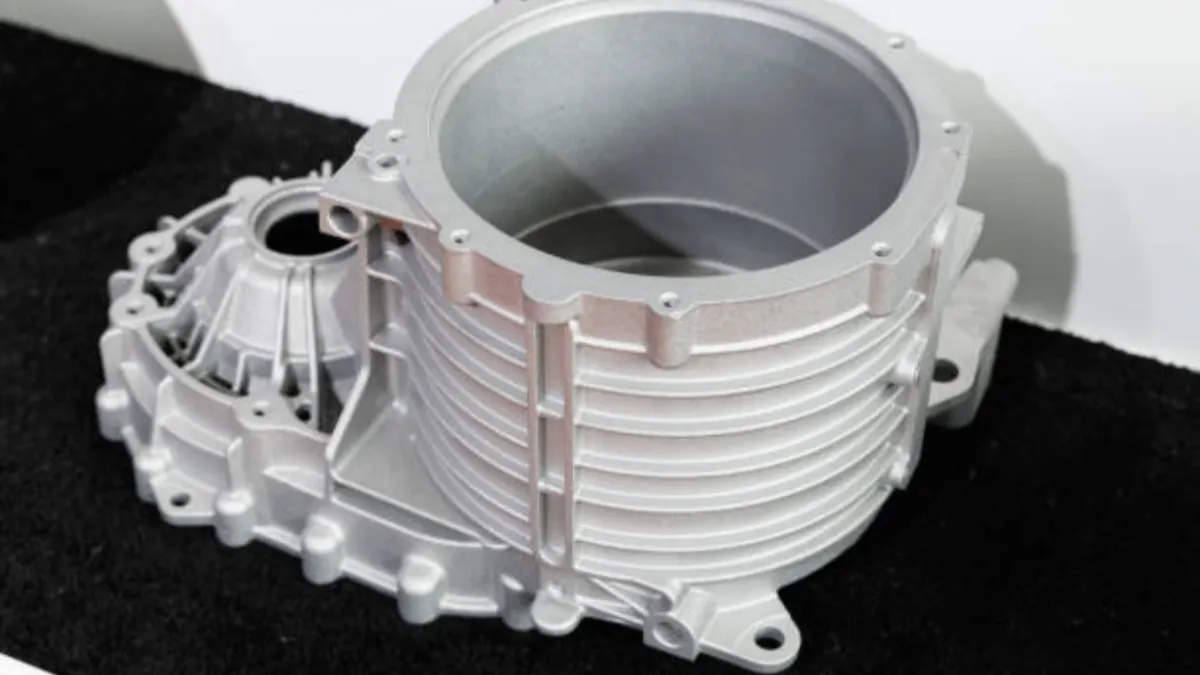
Three service demands push a drawing toward this alloy. Heat is the common one. Under-hood brackets, carcaças de compressor, and engine-adjacent parts want the strength retention a 3-4% copper Al-Si alloy delivers where an A380-style grade would soften. Pressure tightness is the second: the alloy’s feeding behavior and low magnesium suit fluid-handling castings, panelas de óleo, and housings that must pass a leak test. Machinability is the third, since silicon held near the bottom of its band is kinder to cutting edges than the high-silicon die-casting grades.
That combination explains A319’s home turf of engine blocks, panelas de óleo, and similar automotive castings. It also explains something buyers specify less often than they should: A319 is a heat-treatable alloy in practice. T5 aging after a stress-relief, or a full solution-plus-age T6 cycle, moves its mechanical numbers in different directions between strength and elongation. If your specification names A319 aluminum alloy, it should also name the temper. “A319” alone answers the metallurgy question and leaves the heat-treatment question open. O alloy selection guide walks through that property trade-off step by step.
When Standard Metal Still Needs Development
Here is where most eight-week promises die on the first call. Because A319 is a published grade, buyers assume the development content is zero: pick the metal, pour it, ship it. Because A319 sits outside the HPDC mainstream, most die casting suppliers treat it as a quote exception: correct metal, wrong process family. Both views are half right, and the honest frame sorts the work into three routes. O customized alloy buyer guide covers when each route is the right ask.
Route one, pure sourcing. The grade is standard and ingot to it exists on the open market, so the program’s work is verification. Spectrometer readings per heat check the published bands, hydrogen testing precedes the pour, and mechanical coupons come from each trial. Nothing is invented; everything is documented. This route is genuinely short.
Route two, process translation. The part was designed for one casting family and the alloy pulls it into another. Walls that read “thin-wall HPDC” must be re-reviewed for a slower-poured process, and gating, feeding, and shrinkage expectations all move. The machined features at tolerance get a different cost curve. This is development work even though the chemistry is off the shelf, and it is where filling simulation and a real DFM pass earn their keep before steel is cut. O processo de fundição is built around thin-wall fluidity that A319 does not offer.
Route three, chemistry trimming. The standard band is too loose for your duty. Copper is pinned to the top of its range for hot strength, and iron is disciplined below a working ceiling for machining. The whole heat is then verified on a spectrometer. It is still A319 by name, but it becomes a melt-control cooperation with the ingot supplier rather than a catalog order.
A realistic eight-week program is usually route one plus a slice of route two. If the drawing genuinely needs route three, add the supplier’s own trial cadence to the calendar and say so on the first call. The weeks are won by naming the right route early, not by compressing the wrong one.
The Spec-to-Production Plan Week by Week
The schedule below assumes a die-caster-familiar geometry, a standard-grade sourcing route, and a buyer who staffs decisions on the day they are due. Weeks run in sequence, and nothing overlaps without a named risk. The eight-week frame is not a marketing number. The published service track here puts tooling on a 35-day path and production on a 20 to 25-day path. Those two blocks alone total 55 para 60 dias, which is about eight weeks.
Semana 1, specification lock and DFM. Freeze the drawing, the temper call, the acceptance limits for composition and mechanicals, and the leak or X-ray standard if the part is pressure-tight. Send the model in STEP or IGES with 2D tolerances, and ask for the DFM report to come back marked against the three routes above.
Semana 2, citar, agreement, and tooling release. A transparent itemized quote covers metal, processo, acabamento, e ferramentas, with a purchase order behind it. The published track is a quote in two days and a DFM in three, and simple tooling opens on the 35-day path. Complex tooling legitimately stretches that, and any promise that hides the fact is a slogan, not a plan.
Semanas 3 para 7, mold build and melt-side setup. The die is cut, fitted, and trial-shot while the metal side is prepared in parallel. Ingot sourcing is confirmed against the published bands, and the central melting furnace is charged under control. Spectrometer baselines are logged for the heat, and hydrogen readings are taken before each pour. This parallelism is the heart of the schedule, because tooling weeks are free metallurgy time.
Semana 8, first articles, verification, and pilot. Prototype shots come off the tool and into the inspection plan, not into an email attachment with “looks good.” Composition is read per heat on the spectrometer, and a metallographic section confirms the assumed microstructure. X-ray checks internal porosity, CMM covers the critical machined dimensions, and leak testing runs if the part carries a pressure duty. O página de controle de qualidade lists exactly which reports come with this gate. Process tuning and any steel corrections happen here, then a production-rate pilot lot runs the full quality plan and the order hands off to the published 20 to 25-day cadence.
Who Owns Each Week on the Plan
| Estágio | Buyer decides | Foundry delivers |
|---|---|---|
| Spec lock (W1) | Temperamento, acceptance limits, test standard | DFM against the alloy’s process family |
| Quote and PO (W2) | Itemized cost review, tooling terms | Citação em 2 dias, tooling schedule |
| Ferramentas (W3-7) | Weekly progress via MES tracking | Die build, controle de fusão, per-heat logs |
| First articles (W8) | Gate pass or fail within days | Spectrometer, raio X, CMM, leak reports |
| Pilot and handoff (W8) | Sign-off and repeat-order trigger | Full quality plan at production rate |
The schedule breaks in one place more often than any other: the buyer’s own review gate in week eight. Sample approval that takes three weeks turns an eight-week program into eleven with no foundry fault at all. Put your internal review deadline in the PO, name one approver, and hold the discipline of the sample gate.
When This Eight-Week Plan Is the Wrong Plan
Do not run it if the volume cannot carry the tooling and verification cost as a one-off. Route-three melt cooperation stacks supplier trial cycles on top of that arithmetic, and the cost logic is the real decision-maker. O custom-alloy cost and ROI analysis shows how to price that trade honestly. Do not run it as a disguise for a process change nobody has reviewed either. If the geometry says thin-wall HPDC, the right answer is usually an A380 or ADC12 class grade. That is a selection call, not A319 with a schedule excuse.
And do not expect it to absorb a moving drawing. After week two, every change resets the clock it touches. Run the plan when the property logic is honest. Hot strength, estanqueidade à pressão, and machining duty should genuinely point to the Al-Si-Cu corner of the map. Choose a supplier who will say in week one whether your part is route one, two, or three.
Common Questions About A319 Programs
What is A319 aluminum alloy used for?
A319 (ASTM 319.0) is specified for castings that need strength at temperature, estanqueidade à pressão, e usinagem. Typical parts include engine-block-class automotive castings, panelas de óleo, and compressor and fluid-handling housings. Isso é 3.0-4.0% copper is the hot-strength engine, enquanto 5.5-6.5% silicon keeps it castable without choking machinability.
Is A319 the same as A380 for die casting?
Não. Both are Al-Si-Cu casting alloys, but A380 runs more silicon (7.5-9.5%) for thin-wall fluidity in high-pressure die casting. A319’s lower silicon and comparable copper favor hot strength, tightness, and machining in slower processes. Swapping one for the other is a process decision, not a drawing note.
Can an A319 program really reach production in 8 semanas?
Yes for a standard grade sourced and verified on a normal program. The published track is a quote in two days, tooling in 35 dias, and production in 20 para 25 dias, so eight weeks is tight but real. No for proprietary chemistry, which needs ingot-supplier trial cycles on the supplier’s calendar. Name your route before you accept a timeline.
What tests should an A319 program require before production?
Five gates cover the alloy honestly. Composition is verified per heat on a direct-reading spectrometer against the published bands, hydrogen testing checks the melt before pour, and a metallographic section confirms microstructure and temper. X-ray catches internal porosity on pressure-tight parts, and mechanical coupons plus CMM dimensions close the sample gate. Ask for the reports, not assurances.
Considerações Finais
A319 aluminum alloy is a defined metal with real, published limits. The honest question is not whether the grade exists. It is whether your part is a sourcing job, a process translation, or a chemistry trim. Classify that in week one and the eight-week frame holds against the site’s own 35-day tooling and 20 to 25-day production cadence. Bring the frozen specification to the página de contato and the route gets classified on the first reply instead of the fifth.