Why Aluminum Alloy Selection Matters in Die Casting
Choosing the right aluminum alloy is one of the earliest decisions that shapes the cost, quality, and performance of every die cast part. Two castings can come off the same machine, at the same cycle time, and still behave completely differently in the field — because alloy chemistry decides mechanical strength, pressure tightness, corrosion resistance, machinability, and how heat moves through the part.
For sourcing teams and design engineers, the practical problem is that alloy names arrive from three different standard systems. A US buyer may specify A380, a European drawing may call for ENAC 47100, and an Asian supplier quotes ADC12. Understanding how these series relate to each other prevents costly confusion at the RFQ stage. This guide explains the mainstream die casting aluminum alloys — the JIS series (ADC12, ADC1), the ASTM series (A380, A360), and the EN series (ENAC 44300, 47100, 46000) — in plain procurement language.
What Is a Die Casting Aluminum Alloy?
Die casting aluminum alloys are engineered Al-Si family materials designed for high-pressure die casting (HPDC). Silicon is the workhorse element: it lowers the melting point, improves melt fluidity so thin walls fill cleanly, and reduces solidification shrinkage. Copper adds strength and machinability but costs corrosion resistance. Iron, magnesium, and manganese round out the chemistry in smaller amounts.
Nearly all structural die castings today come from the Al-Si-Cu family, standardized under three parallel systems:
- JIS H5302 (Japan) — the ADC series, the default commercial language across Asian die casting suppliers.
- ASTM B85 (US) — the A-series: A360, A380, A383, A413 and others.
- EN 1706 (Europe) — the ENAC designation system, such as ENAC 44300 (AlSi12(Fe)).
The families overlap heavily, which is why cross-referencing them — rather than treating each standard as a separate material — is the faster way to a sound decision.
The JIS Series: ADC12, ADC1, and DC1
ADC12 is the single most widely used die casting aluminum alloy in Asia, and for good reason. With silicon at 9.6–12.0% and copper at 1.5–3.5%, it delivers a typical tensile strength around 310 MPa, excellent castability, and a balanced cost profile. It is the default choice for housings, brackets, heat sinks, and general structural components. BIAN runs ADC12 as its mainstay alloy for die cast housings and parts, including environmentally compliant ingot grades for export programs.
ADC1 sits at the high-silicon end (Si 11.0–13.0%) with copper held below 0.6%. The result is superior melt fluidity and pressure tightness, at somewhat lower strength than ADC12. Thin-walled enclosures and parts that must pass leak tests are its natural territory. DC1 covers the same high-Si, low-Cu chemistry in Chinese commercial usage, alongside the GB equivalent YL102.
The ASTM Series: A380 and A360
A380 is the best-known die casting alloy in the North American market. Its chemistry (Si 7.5–9.5%, Cu 3.0–4.0%) produces the best machinability of the common alloys and a typical tensile strength near 320 MPa. Gear cases, valve bodies, and any part that needs post-casting machining are classic A380 applications. Its trade-off is lower corrosion resistance than low-copper grades.
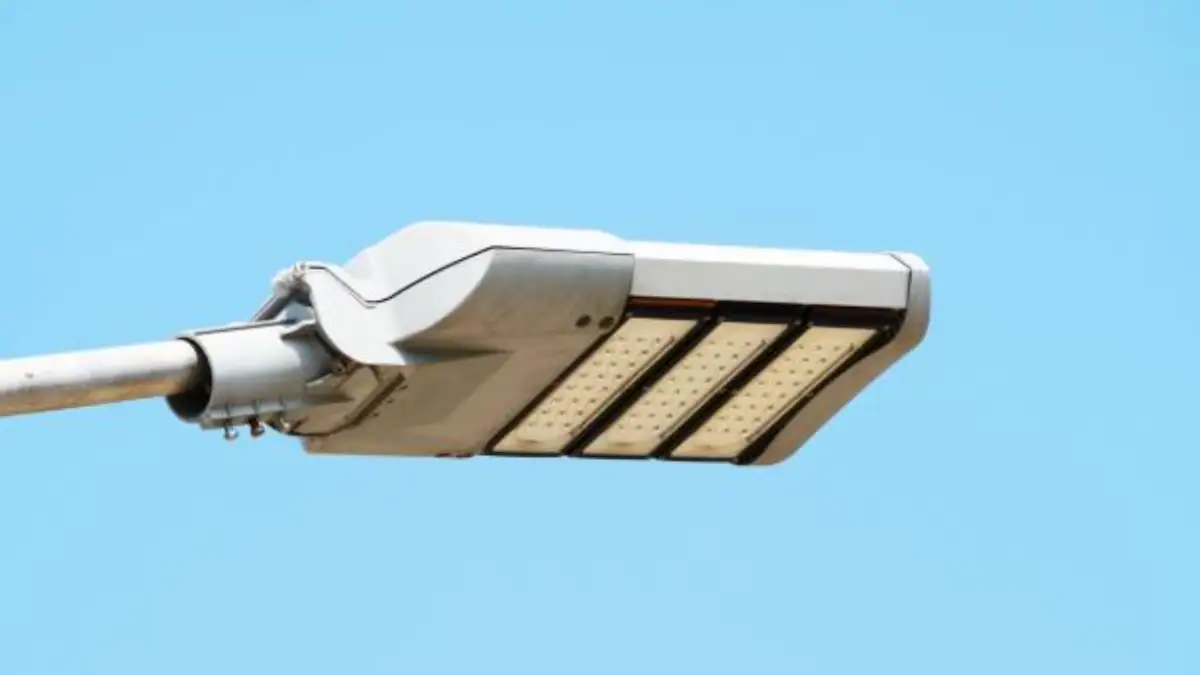
A360 keeps silicon high (9.0–10.0%) and copper below 0.6%, giving better corrosion resistance and slightly higher ductility than A380, at the cost of somewhat harder machining. Thin-walled parts exposed to weather — outdoor luminaire housings, marine-adjacent components — often land on A360 or its low-copper equivalents.
The EN Series: ENAC 44300, 47100, and 46000
European drawings use the ENAC numbering from EN 1706. The three grades that appear most often in die casting RFQs are:
- ENAC 44300 — AlSi12(Fe): high fluidity, excellent pressure tightness, and strong thin-wall capability. The European workhorse for housings and sealed enclosures.
- ENAC 47100 — AlSi10Cu2(Fe): the closest EN match to ADC12; a general-purpose structural alloy balancing strength and castability.
- ENAC 46000 — AlSi9Cu3(Fe): the EN counterpart to A380, favored where machinability matters.
If your drawing cites one ENAC grade and a supplier quotes a JIS or ASTM name, the equivalence table below tells you whether the substitution is a genuine match or a downgrade hiding in different nomenclature.
Alloy Comparison at a Glance
| Alloy | Standard | Si (%) | Cu (%) | UTS (typical) | Best Known For |
|---|---|---|---|---|---|
| ADC12 | JIS H5302 | 9.6–12.0 | 1.5–3.5 | ~310 MPa | General-purpose castability and cost balance |
| A380 | ASTM B85 | 7.5–9.5 | 3.0–4.0 | ~320 MPa | Best machinability; machined components |
| A360 | ASTM B85 | 9.0–10.0 | ≤0.6 | ~300 MPa | Corrosion resistance; thin walls |
| ENAC 44300 | EN 1706 | 10.5–13.5 | ≤0.3* | ~240 MPa | Fluidity and pressure tightness |
| ADC1 / DC1 | JIS / GB | 11.0–13.0 | ≤0.6 | ~290 MPa | Leak-critical thin-wall enclosures |
*Other alloying elements differ by grade; see the governing standard for full chemistry. Values are typical high-pressure die cast figures — always confirm against the mill certificate and your supplier’s spectrometer report for each lot.
Cross-Standard Equivalence: Which Alloy Matches Which?
The three naming systems describe overlapping materials. The three equivalence anchors that settle most RFQ discussions:
| Family | JIS | ASTM | EN | GB / BS | Character |
|---|---|---|---|---|---|
| General structural | ADC12 | A383 | ENAC 47100 | YL113 | Best all-round castability |
| Machining-friendly | — | A380 | ENAC 46000 | YL112 | Highest strength, easy machining |
| Fluid / leak-tight | ADC1 | A413 | ENAC 44300 | YL102 / LM6 | Thin walls, pressure tightness |
Two cautions apply. First, “equivalent” means close, not identical — impurity limits and minor elements differ between standards, so critical parts still need a first-article inspection on the actual chemistry. Second, when a drawing cites a corrosion-critical grade such as A360, substituting a high-copper alloy like A380 is not an equivalent swap even when strength numbers look similar.
Specialty High-Thermal-Conductivity Alloys: AlSi8, LHB1, HA7-S
Standard die casting alloys conduct heat at roughly 90–150 W/(m·K) — adequate for most housings, but a bottleneck for LED lighting and EV electronics where heat must leave the part fast. That gap drove the development of specialty high-conductivity die casting alloys: the AlSi8 family and grades such as LHB1 and HA7-S, which push thermal conductivity up to 200 W/(m·K) while remaining fully die-castable.
For LED luminaire housings, battery tray components, power electronics enclosures, and motor controller housings, these grades can eliminate downstream heat sinks or reduce them substantially. The trade-off is typically somewhat lower strength than structural grades, so part geometry and wall sections need to be engineered around the alloy rather than copied from an ADC12 design. BIAN regularly casts AlSi8, LHB1, and HA7-S for LED and new-energy-vehicle programs, with in-house spectrometer verification on every melt.
How to Match an Alloy to Your Application
A short decision path covers most projects:
- General housings and brackets — start with ADC12 (or A383 / ENAC 47100 on the drawing). It is the safest default and the easiest to source.
- Parts that will be machined — A380 / ENAC 46000 cut faster and cleaner.
- Outdoor or corrosion-exposed enclosures — lean toward A360 or low-copper grades, then add powder coating or e-coating for severe environments.
- Thin walls and leak-tested parts — high-Si, high-fluidity grades: ADC1, A413, ENAC 44300.
- Heat-dissipating parts — AlSi8, LHB1, or HA7-S when standard alloys cannot move enough heat.
Application context matters as much as the datasheet. The same ENAC 44300 housing behaves differently behind a powder-coated outdoor luminaire than inside a sealed automotive controller — which is why experienced suppliers ask about the part’s environment before confirming an alloy. You can see how alloy choice interacts with process capabilities on the full die casting capability overview.
What Buyers Should Verify Before Ordering
Alloy substitution is one of the quietest failure modes in die casting procurement. A part that measures correctly and still fatigues early usually traces back to chemistry that drifted from the specified grade. Four checks close that gap:
- Melt-level verification, not just ingot certificates. Ask how often the supplier tests the actual melt. Spectrometer checks every two hours — the cadence BIAN runs on its die casting lines — catch contamination and composition drift long before it reaches a casting.
- Lot-matched mill certificates. Certificates should correspond to the delivered lot and cite the governing standard (JIS H5302, ASTM B85, or EN 1706).
- First-article chemistry report alongside dimensional reports for any new part or alloy change.
- Remelt discipline. A supplier with a centralized melting and refining operation for return material — rather than ad-hoc remelting at the machine — maintains tighter chemistry consistency across production runs.
Buyers planning multi-year programs should also confirm that the supplier’s quality system (ISO 9001 for general manufacturing, IATF 16949 for automotive) covers material control, not just final inspection.
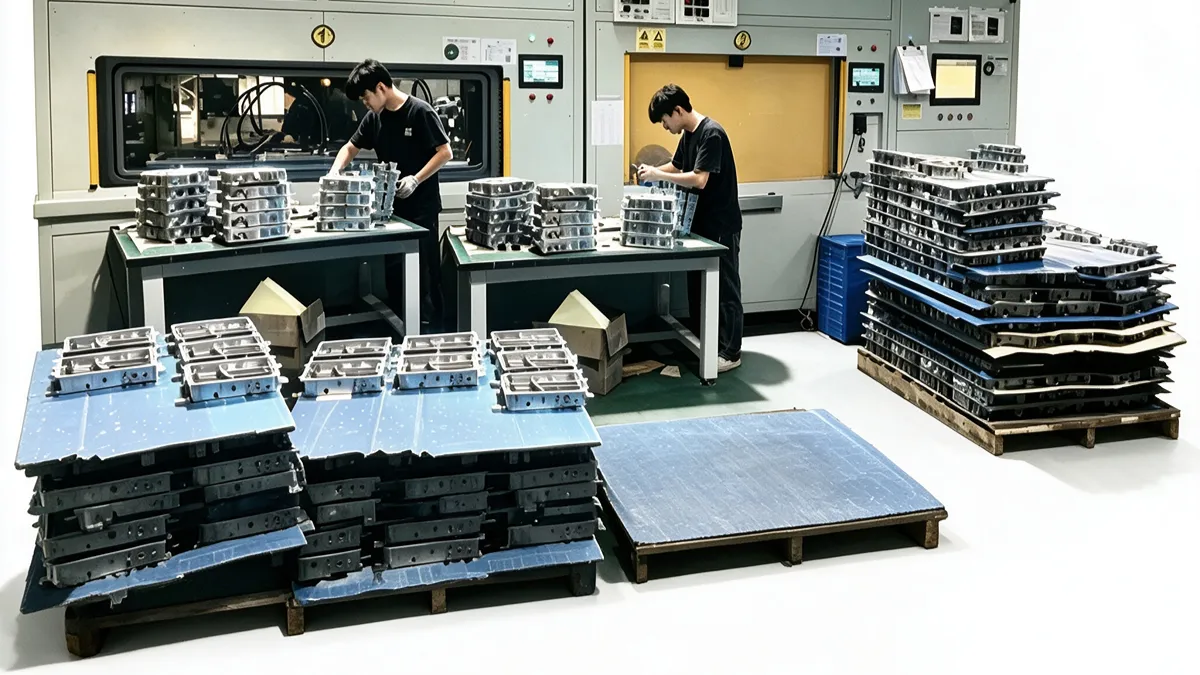
From Alloy Choice to Production Reality
Alloy selection is where a die casting project starts, but the outcome still depends on tooling, machine tonnage, and process control. A supplier who can discuss the interaction among alloy fluidity, gate design, and wall thickness — and show you melt records — will save more cost over a program than a marginal difference in ingot price ever will. For a broader view of the casting workflow, see our overview of the aluminum die casting process.
If your drawing specifies a grade outside this list — a national standard, a customer-specific alloy, or a high-conductivity variant — submit the drawing for review. Alloy ranges from the common ADC12 through specialty grades are regularly cast in production, and engineering feedback on the alloy-to-part fit is available before tooling starts. Request a quote through the contact page to start the conversation.
FAQ
Which aluminum alloy is best for die casting?
ADC12 (JIS), A383 (ASTM), and ENAC 47100 (EN) are the most common general-purpose choices because they combine good castability, around 300 MPa typical strength, and competitive cost. Parts needing machining often shift to A380, while corrosion-exposed enclosures favor A360 or another low-copper grade.
Is ADC12 the same as A380?
No. ADC12’s closest ASTM equivalent is A383, not A380. A380 carries more copper (3.0–4.0%), which improves machinability but reduces corrosion resistance. For most housings the two families are interchangeable in practice, but for corrosion-critical or leak-critical parts the distinction matters.
Which die casting alloy has the highest thermal conductivity?
Specialty grades such as AlSi8, LHB1, and HA7-S reach up to 200 W/(m·K), well above the 90–150 W/(m·K) typical of standard Al-Si die casting alloys. They are used for LED housings, power electronics, and EV components where heat dissipation drives the design.
What should buyers verify about alloy composition before ordering?
Ask for melt-level spectrometer testing frequency (ideally every two hours), lot-matched mill certificates citing JIS H5302 / ASTM B85 / EN 1706, a first-article chemistry report for new parts, and confirmation of centralized remelt control. These checks prevent quiet alloy substitution during production.